Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Efficient and reliable transportation of coal ash particles is crucial in industrial applications, particularly in power plants and waste management facilities. The choice of conveying method significantly impacts operational efficiency, cost-effectiveness, and environmental compliance. This article provides a detailed comparison of common coal ash particle conveying methods, focusing on their mechanisms, advantages, and applications. The information is presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions based in China.
About HeadPowder Engineering
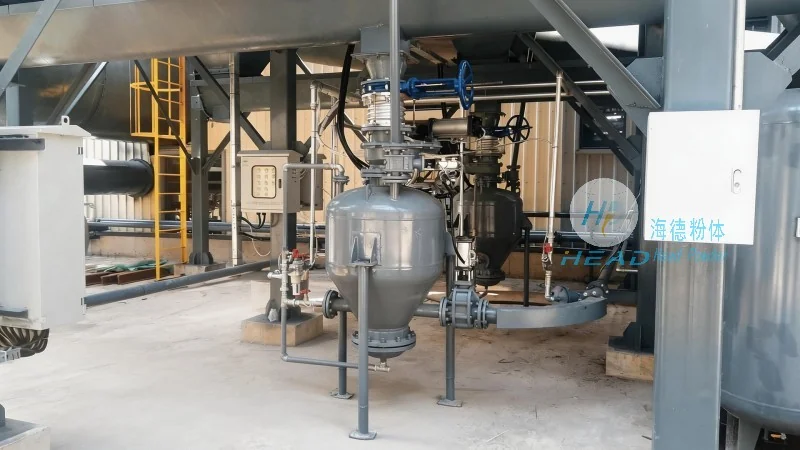
Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) specializes in designing and manufacturing advanced conveying systems tailored to the unique requirements of coal ash handling. With years of experience in the industry, HeadPowder offers a range of solutions that ensure safe, efficient, and cost-effective transport of coal ash particles. The company's headquarters is located in Shandong, China, and it serves clients globally with customized conveying equipment.
1. Screw Conveyors for Coal Ash Particle Transport
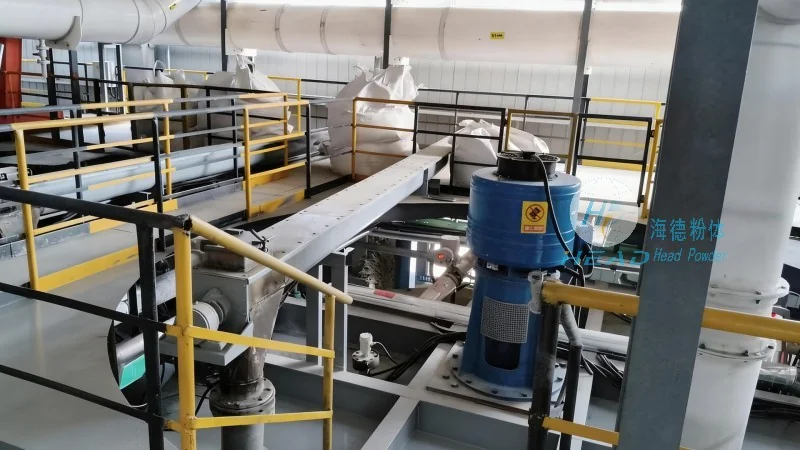
Screw conveyors, also known as auger conveyors, are widely used for transporting coal ash particles due to their simplicity and reliability. This type of conveyor consists of a rotating screw (auger) inside a cylindrical housing. As the screw rotates, it pushes the coal ash particles forward along the length of the conveyor. The design allows for vertical and horizontal transport, making it suitable for various applications, including material feeding, batching, and transfer between processes. Screw conveyors are particularly effective for handling dry coal ash with low to moderate moisture content. They are easy to install, maintain, and operate, which reduces downtime and maintenance costs. HeadPowder offers screw conveyors with adjustable speed controls and variable pitch screws to optimize material flow and prevent blockages. The company's models are constructed from corrosion-resistant materials, ensuring durability in harsh environments.
2. Pneumatic Conveying Systems for Coal Ash
Pneumatic conveying systems use air or other gases to transport coal ash particles through a pipeline network. This method is ideal for applications requiring high flexibility, as the conveying lines can be easily reconfigured to adapt to changing operational needs. Pneumatic systems are available in two main types: pressure and vacuum. Pressure systems push the material through the pipeline using compressed air, while vacuum systems draw the material into the pipeline using a vacuum pump. Both types offer advantages in terms of material handling, such as the ability to transport coal ash over long distances and through multiple bends. However, pneumatic conveying can be more energy-intensive compared to other methods, and it may require additional filtration to prevent dust emissions. HeadPowder provides pneumatic conveying systems with high-efficiency filters and adjustable air pressure controls to ensure optimal performance and compliance with environmental regulations. The company's systems are designed to handle a wide range of coal ash particle sizes and moisture levels, making them versatile for various industrial applications.
3. Belt Conveyors for Bulk Coal Ash Transport
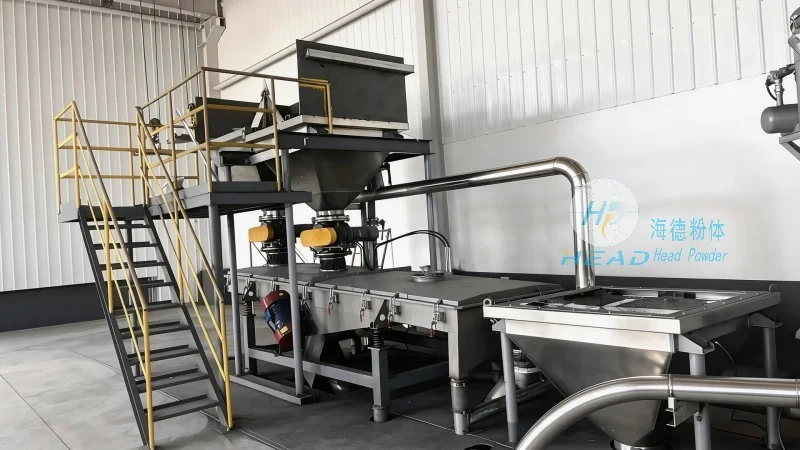
Belt conveyors are a classic and widely adopted method for transporting bulk coal ash over long distances. This system consists of a continuous belt that moves over rollers or pulleys, carrying the coal ash from the source to the destination. Belt conveyors are highly efficient for high-volume transport, with the ability to handle large quantities of material at a time. They are suitable for both horizontal and inclined transport, and can be integrated with other equipment, such as feeders and elevators, to form a complete conveying system. The primary advantages of belt conveyors include high capacity, low maintenance, and the ability to operate continuously for extended periods. However, belt conveyors require regular inspection and maintenance to prevent belt wear and tear, and they may not be suitable for transporting coal ash with high moisture content, as it can cause the belt to slip or become damaged. HeadPowder manufactures belt conveyors with reinforced belts and advanced tensioning systems to ensure long service life and reliable operation. The company's models are available in various widths and lengths to accommodate different production requirements.
4. Bucket Elevators for Vertical Coal Ash Transport
Bucket elevators are specifically designed for vertical transport of coal ash particles, making them essential in applications where material needs to be lifted to elevated levels, such as in storage silos or processing facilities. This system consists of a vertical or inclined conveyor with a series of buckets attached to a chain or belt. As the buckets move up the conveyor, they scoop up the coal ash and discharge it at the top. Bucket elevators are known for their high capacity and ability to handle vertical lifts of up to several hundred feet. They are particularly effective for transporting coal ash with high moisture content or sticky materials, as the buckets can effectively lift and discharge the material without clogging. However, bucket elevators require careful design to ensure proper bucket spacing and chain tension to prevent material spillage and equipment damage. HeadPowder offers bucket elevators with adjustable bucket spacing and variable speed controls to optimize material flow and prevent blockages. The company's models are constructed from wear-resistant materials, ensuring durability in harsh operating conditions.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu