Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Efficient and eco-friendly material handling is a critical concern for industries dealing with bulk materials. Traditional methods like belt conveyors or bucket elevators often face challenges such as dust pollution, high energy consumption, and operational inefficiencies. This is where dust air conveying technology steps in as a superior alternative, offering a solution that not only enhances productivity but also prioritizes environmental sustainability.
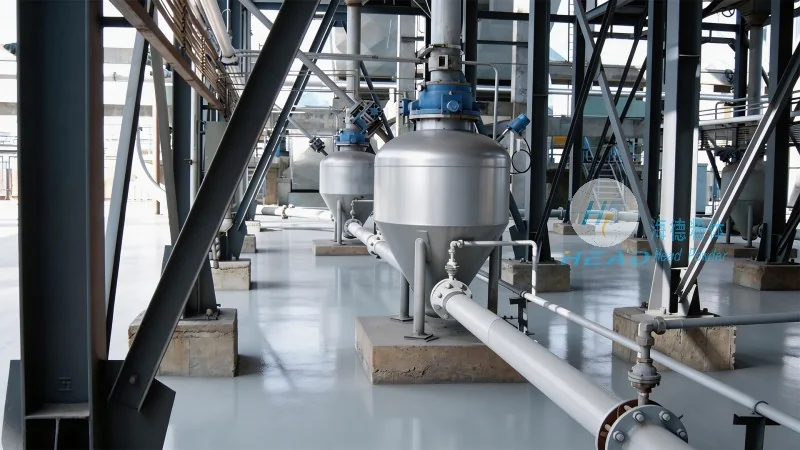
Understanding Dust Air Conveying Technology
Dust air conveying, also known as pneumatic conveying, is a method of transporting bulk materials using a stream of air under pressure or vacuum. Unlike mechanical systems that rely on physical contact and friction, this technology utilizes air to move materials through pipelines. The process involves feeding material into a hopper, which then transfers it into a pipeline where it is carried by the air flow to the destination point. This method is particularly effective for handling fine powders, granules, and other dusty materials, making it ideal for industries like pharmaceuticals, food processing, and chemical manufacturing.
HeadPowder's Advanced Air Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in developing cutting-edge dust air conveying systems tailored to meet diverse industrial needs. The company's solutions are engineered to deliver high efficiency, low maintenance costs, and minimal environmental impact. HeadPowder's air conveying systems are designed with advanced components such as high-efficiency blowers, robust pipelines, and intelligent control systems that ensure smooth and reliable material transport. By leveraging their expertise in material handling engineering, HeadPowder provides customized solutions that optimize workflow and reduce operational costs for clients worldwide.
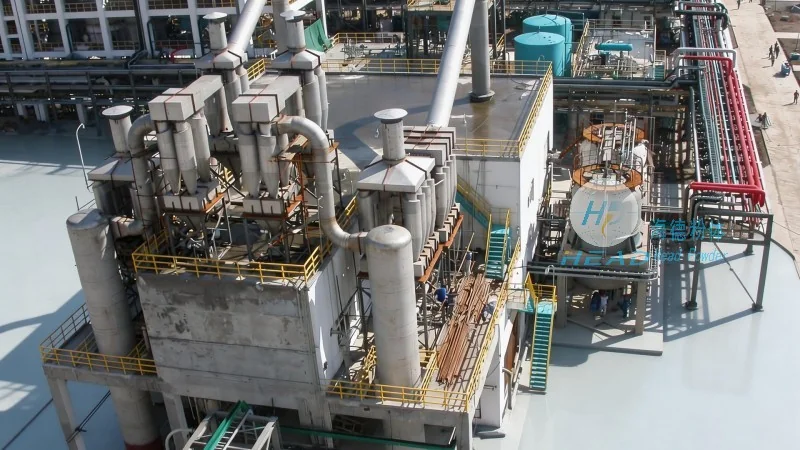
Key Advantages of Dust Air Conveying
Compared to traditional material handling methods, dust air conveying offers several distinct advantages. First, it significantly reduces dust emissions, contributing to a cleaner and safer working environment. This is achieved through enclosed systems that contain the material within the pipeline, preventing dust from escaping into the air. Second, the technology is highly energy-efficient, as it minimizes energy loss compared to mechanical systems that require constant friction and movement. Third, it allows for flexible and compact installations, as the pipelines can be routed through existing structures without the need for large machinery or extensive space. Additionally, the system is easy to maintain, with fewer moving parts and lower risk of mechanical failure. These advantages make dust air conveying an attractive option for industries looking to improve their operational efficiency while adhering to environmental regulations.
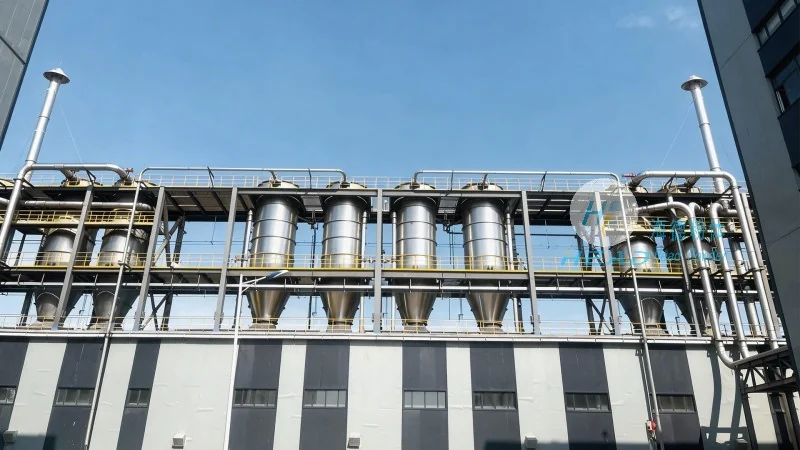
Applications in Various Industries
The versatility of dust air conveying makes it applicable across a wide range of industries. In the pharmaceutical industry, for example, it is used to transport fine powders and granules with strict hygiene requirements, ensuring that the materials remain clean and free from contamination. In food processing, the technology is employed to handle ingredients like flour, sugar, and spices, maintaining product quality and safety standards. The chemical industry also benefits from this technology, as it allows for the safe and efficient transport of hazardous materials without exposing workers to dangerous conditions. Furthermore, in the agricultural sector, dust air conveying is used to move grains and other bulk crops, improving storage and processing efficiency. HeadPowder's systems are designed to adapt to these diverse applications, providing reliable performance in each sector.
Customization and Integration Capabilities
HeadPowder understands that every industrial operation has unique requirements. Therefore, their air conveying solutions are highly customizable to fit specific processes and space constraints. The company offers a range of system configurations, including pressure and vacuum conveying, to accommodate different material types and transport distances. Additionally, HeadPowder provides integration services to seamlessly connect the air conveying system with existing production lines, ensuring smooth operation and minimal disruption. Their team of engineers works closely with clients to assess their needs, design a tailored solution, and provide ongoing support to ensure optimal performance. This commitment to customization and integration sets HeadPowder apart as a trusted partner in material handling solutions.
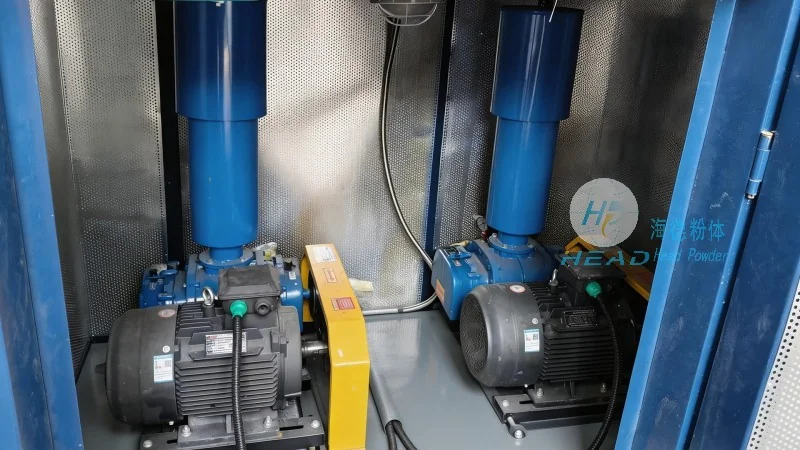
Environmental and Operational Benefits
From an environmental perspective, dust air conveying is a sustainable choice for industries aiming to reduce their carbon footprint. By minimizing dust emissions and energy consumption, the technology aligns with global efforts to promote eco-friendly practices. This not only helps companies comply with environmental regulations but also enhances their corporate social responsibility. Operationally, the system offers cost savings through reduced maintenance, lower energy bills, and increased productivity. The enclosed design of the system also reduces the risk of material loss and contamination, which can be costly in industries where product quality is paramount. Overall, the combination of environmental and operational benefits makes dust air conveying a smart investment for any business looking to enhance its material handling capabilities.
Conclusion: The Future of Material Handling
As industries continue to evolve and demand more efficient and sustainable solutions, dust air conveying technology remains a key player in the material handling landscape. With its ability to deliver high performance while minimizing environmental impact, this technology is well-positioned to meet the challenges of the future. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this technology, providing advanced solutions that help industries achieve their operational goals. By choosing dust air conveying, businesses can improve their productivity, reduce costs, and contribute to a greener future. The future of material handling is indeed in the air, and HeadPowder is leading the way.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu