Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Efficient and environmentally friendly material handling solutions are crucial in the modern agricultural and industrial sectors, particularly when dealing with bulk materials like ammonia fertilizer. Traditional methods such as truck or conveyor belt transport often face challenges related to cost, safety, and environmental impact. This is where airborne transport technology, specifically designed for ammonia fertilizer, emerges as a superior alternative. By leveraging the principles of pneumatic conveying, this method offers a seamless way to move large quantities of fertilizer while minimizing operational costs and reducing ecological footprint.
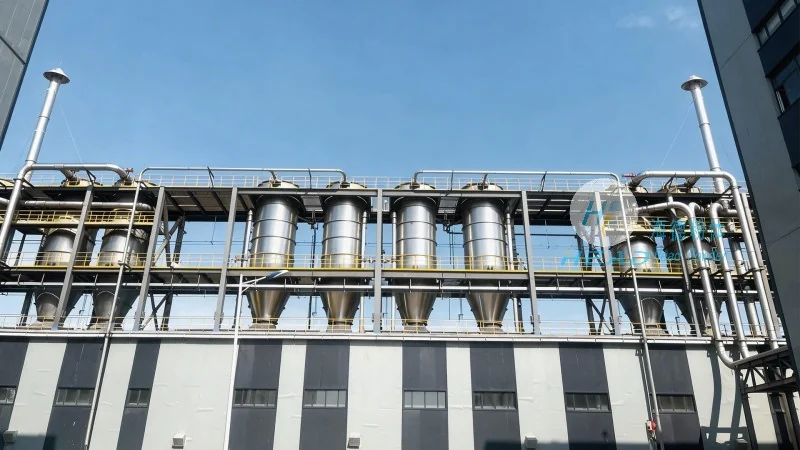
Understanding Airborne Transport for Ammonia Fertilizer
At its core, airborne transport of ammonia fertilizer involves the use of compressed air to move material through a pipeline system. Unlike traditional mechanical conveyors, this method eliminates the need for moving parts that can wear out or require frequent maintenance. The process typically starts with the fertilizer being fed into a hopper, where it is then drawn into a pipeline by the force of the air. The air-fertilizer mixture travels through the pipeline to the destination point, where it is separated and deposited. This technology is particularly effective for handling fine powders and granules, ensuring consistent and reliable delivery.
The Advantages of Airborne Transport
One of the key benefits of using airborne transport for ammonia fertilizer is its efficiency. The system can handle large volumes of material with minimal labor, reducing the need for manual handling and associated risks. Additionally, the process is highly automated, allowing for precise control over the flow rate and destination of the fertilizer. This not only improves operational efficiency but also enhances safety in the workplace by eliminating the need for workers to handle heavy or potentially hazardous materials directly.
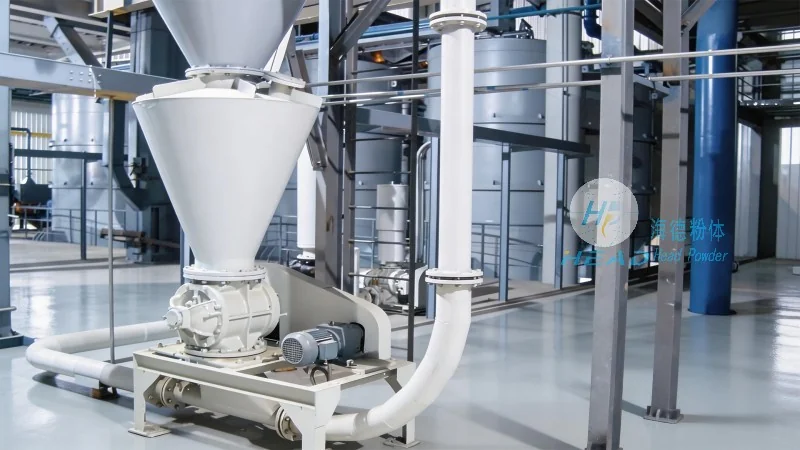
From an environmental perspective, airborne transport is a more sustainable option. By reducing the reliance on trucks and other vehicles, the method lowers carbon emissions and air pollution. The closed pipeline system also prevents dust and other pollutants from being released into the environment, contributing to better air quality. Furthermore, the energy consumption of the system is optimized, making it a cost-effective and eco-friendly solution for bulk material transport.
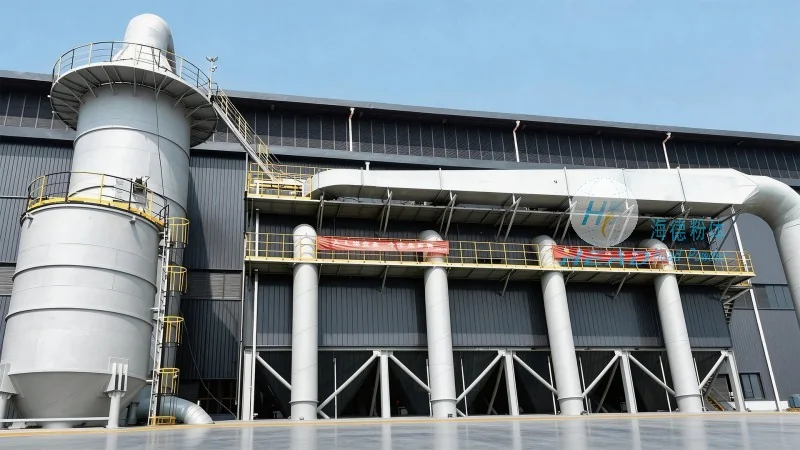
HeadPowder Engineering: Your Partner in Efficient Fertilizer Transport
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions, specializing in airborne transport systems for ammonia fertilizer. With years of experience in the industry, HeadPowder has developed cutting-edge technology that meets the highest standards of efficiency and environmental responsibility. The company's commitment to innovation and customer satisfaction has made it a trusted name in the agricultural and industrial sectors.
HeadPowder's airborne transport systems are designed to be customized to meet the specific needs of each client. Whether it's a small-scale operation or a large industrial facility, the company offers tailored solutions that optimize material flow, reduce costs, and enhance safety. The team at HeadPowder works closely with clients to understand their unique requirements and develop a system that delivers the best possible results.
Key Features of HeadPowder's Airborne Transport Solutions
HeadPowder's airborne transport systems for ammonia fertilizer are equipped with several advanced features that set them apart from traditional methods. The systems utilize high-quality materials and components that are resistant to corrosion and wear, ensuring long-term durability and reliability. The control systems are sophisticated, allowing for real-time monitoring and adjustment of the transport process. This ensures that the system operates at peak efficiency and minimizes downtime.
Another important feature is the system's flexibility. HeadPowder's solutions can be easily integrated with existing infrastructure, reducing the need for major construction or modifications. The company also provides comprehensive maintenance and support services, ensuring that the system remains in optimal condition throughout its lifespan. This includes regular inspections, repairs, and upgrades as needed, providing clients with peace of mind and continuous performance.
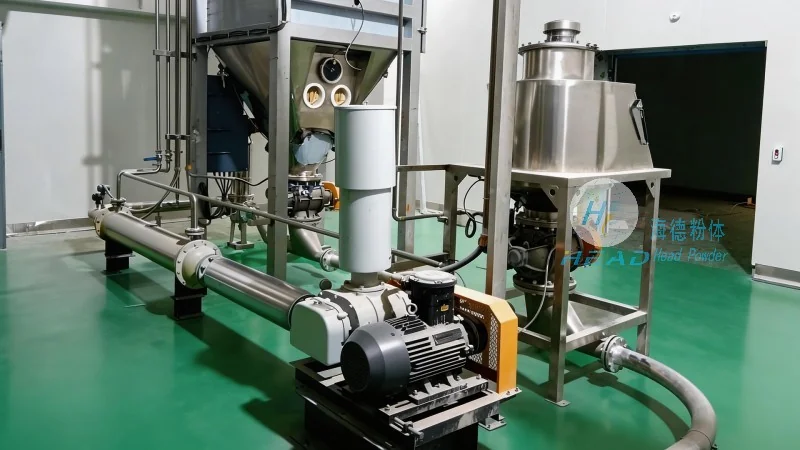
Conclusion: Choosing the Right Material Handling Solution
For businesses looking to improve their material handling processes, especially when dealing with ammonia fertilizer, airborne transport offers a compelling solution. The combination of efficiency, environmental benefits, and safety makes it an attractive option for both new and existing operations. With HeadPowder Engineering as a partner, companies can leverage the latest technology to achieve their goals while maintaining a commitment to sustainability and operational excellence.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu