Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
For industries dealing with mineral and sand materials, efficient and reliable material handling is crucial. Traditional methods like belt conveyors or bucket elevators often face challenges such as material degradation, dust generation, and operational inefficiencies. Pneumatic conveying offers a modern solution that addresses these issues while promoting sustainability. This article explores the benefits and applications of pneumatic conveying systems for transporting mineral and sand materials, highlighting how they contribute to operational efficiency and environmental protection.
The Advantages of Pneumatic Conveying Systems
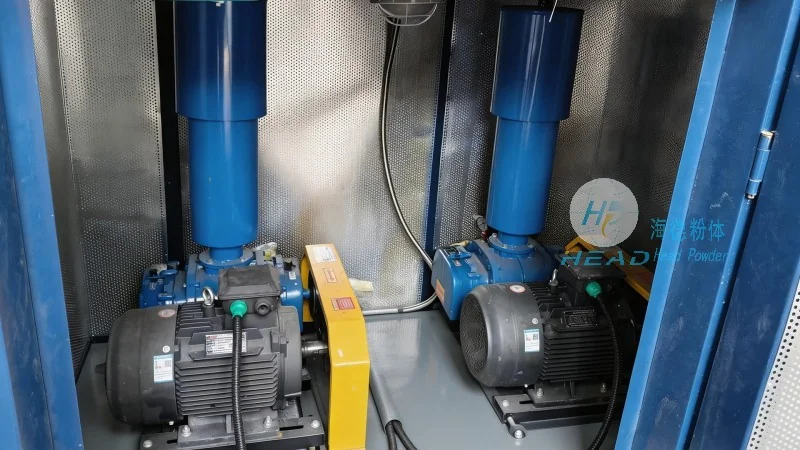
Pneumatic conveying systems utilize air or gas to transport bulk materials like mineral powders and sand particles. Unlike mechanical systems, they eliminate the need for moving parts in contact with the material, reducing wear and tear and extending equipment lifespan. This results in lower maintenance costs and higher uptime. Additionally, pneumatic conveyors can handle a wide range of material properties, including abrasive or corrosive substances, making them versatile for various industrial applications. The system's ability to transport materials in a closed loop also minimizes dust emissions, contributing to a cleaner working environment and compliance with environmental regulations.
Efficiency in Material Transport and Processing
One of the key advantages of pneumatic conveying is its high transport efficiency. By using air pressure to move materials, the system can achieve rapid and continuous material flow, which is essential for high-throughput operations. This is particularly beneficial in mining and construction industries where large volumes of sand and mineral powders need to be moved quickly. The system's ability to handle both dry and wet materials, as well as different particle sizes, ensures flexibility in processing. Moreover, pneumatic conveyors can be integrated with other processing equipment, such as classifiers or mixers, to streamline production workflows and enhance overall productivity.
Environmental Benefits and Sustainability
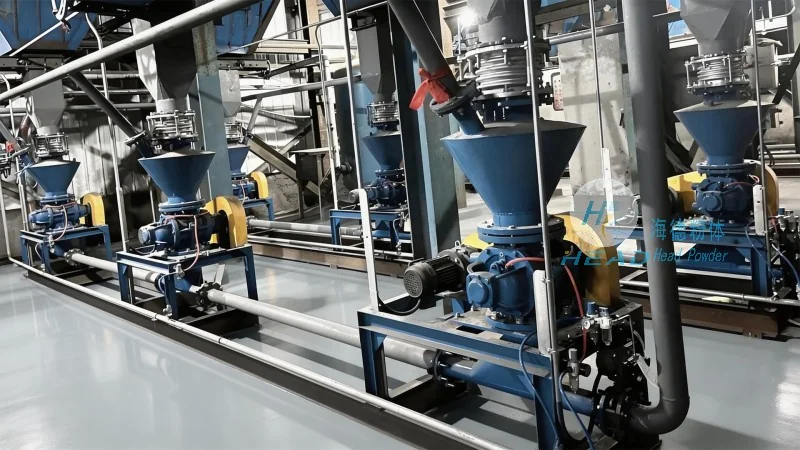
In today's industrial landscape, environmental sustainability is a top priority. Pneumatic conveying systems excel in this aspect by reducing dust pollution and minimizing the need for water or other cleaning agents. The closed system design prevents material spillage and dust dispersion into the air, which is a significant concern with open conveyor systems. This not only improves workplace safety but also helps companies meet environmental standards and reduce their carbon footprint. Furthermore, the energy efficiency of pneumatic conveyors, especially when using optimized air flow and pressure control, contributes to lower operational costs and reduced energy consumption over time.
Application Examples in Mining and Construction
Pneumatic conveying is widely used in the mining industry for transporting crushed minerals and sand from processing plants to storage facilities or for further processing. In construction, it is employed to move sand, cement, and other building materials to different sites or storage areas. The system's ability to handle abrasive materials without causing wear on the equipment makes it ideal for these applications. For example, in a mining operation, a pneumatic conveyor can transport crushed ore from a crusher to a conveyor belt or storage silo, ensuring a smooth and continuous supply of materials for downstream processes. Similarly, in a construction site, the system can deliver sand and cement to mixing plants or storage silos, supporting efficient project execution.
Customization and Scalability of Pneumatic Conveying Systems
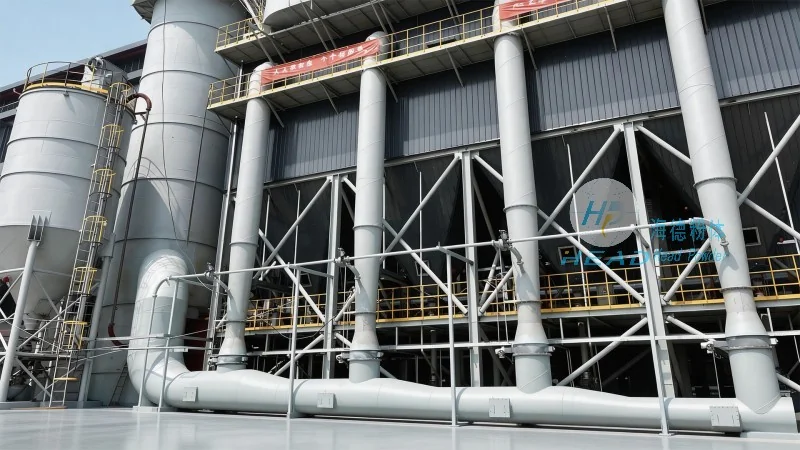
HeadPowder Engineering, a leading provider of material handling solutions, offers customized pneumatic conveying systems tailored to specific industry needs. With decades of experience in the field, the company understands the unique requirements of each client and designs systems that meet their operational and environmental goals. Whether it's a small-scale system for a laboratory or a large-scale system for an industrial plant, HeadPowder Engineering can provide solutions that are scalable and adaptable. The company's team of engineers works closely with clients to assess their material characteristics, transport distances, and operational constraints, ensuring that the final system is optimized for performance and efficiency. This customization approach ensures that clients receive a system that is not only effective but also cost-effective and sustainable.
Conclusion: Choosing the Right Material Handling Solution
For industries dealing with mineral and sand materials, pneumatic conveying offers a superior alternative to traditional mechanical systems. Its efficiency, environmental benefits, and versatility make it an ideal choice for modern industrial operations. By investing in a pneumatic conveying system from HeadPowder Engineering, companies can enhance their operational performance, reduce costs, and contribute to a more sustainable future. With the company's expertise and commitment to quality, clients can trust that their material handling needs will be met with reliable and innovative solutions. As the demand for efficient and eco-friendly material transport continues to grow, pneumatic conveying remains a key technology in the industry, and HeadPowder Engineering is at the forefront of providing these solutions.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu