Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
When it comes to handling anhydrous sodium sulfate, the choice of material transport method can significantly impact operational efficiency, safety, and environmental compliance. Airflow transport, or pneumatic conveying, has emerged as a leading solution for transporting this chemical efficiently while minimizing environmental impact. This article explores the benefits and applications of airflow transport systems specifically designed for anhydrous sodium sulfate, highlighting how companies like Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) are leveraging this technology to enhance material handling processes.
Understanding Anhydrous Sodium Sulfate and Its Handling Requirements
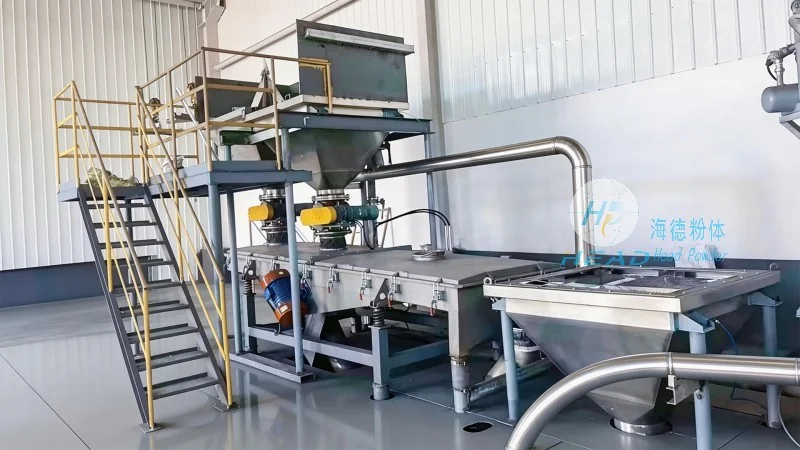
Anhydrous sodium sulfate, also known as sodium sulfate anhydrous (Na₂SO₄), is a white crystalline powder commonly used in various industrial applications, including glass manufacturing, detergents, and chemical synthesis. Due to its fine particle size and potential for dust generation, traditional bulk handling methods such as belt conveyors or manual loading can pose challenges related to dust control, material loss, and operational safety. Airflow transport systems address these challenges by using compressed air or other gases to move the material through a sealed pipeline network, ensuring a clean, dust-free transfer process.
The Advantages of Airflow Transport for Anhydrous Sodium Sulfate
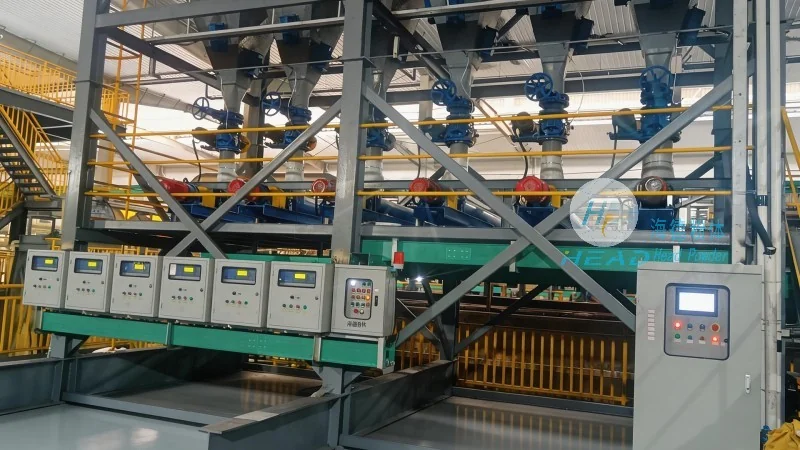
HeadPowder specializes in designing and implementing advanced airflow transport solutions tailored to the unique characteristics of anhydrous sodium sulfate. The primary benefits of this technology include: enhanced material handling efficiency, reduced operational costs, improved safety through dust containment, and minimized environmental impact. By eliminating the need for manual handling and open-air transfer, airflow systems prevent dust exposure, which is crucial for maintaining workplace safety standards. Additionally, the sealed pipeline design reduces material spillage and contamination, ensuring product integrity throughout the transport process.
Key Features of HeadPowder's Airflow Transport Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers comprehensive airflow transport systems that incorporate several key features to optimize performance for anhydrous sodium sulfate. These systems typically include: high-capacity pneumatic conveyors with adjustable air pressure and flow rates, dust collection and filtration units to ensure compliance with air quality regulations, and automated control systems for seamless integration with existing production lines. The company’s expertise lies in customizing these solutions to meet specific client requirements, such as varying material flow rates, pipeline lengths, and environmental standards.
Environmental and Operational Benefits
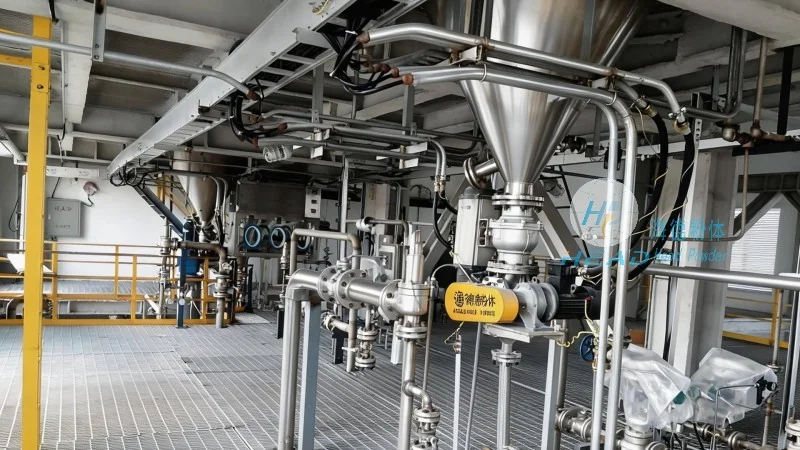
From an environmental perspective, airflow transport significantly reduces the carbon footprint associated with material handling by minimizing energy consumption compared to traditional methods. The sealed system also prevents dust emissions, contributing to cleaner air quality in industrial settings. Operationally, these systems offer consistent performance with minimal downtime, as they eliminate the need for frequent maintenance associated with mechanical conveyors. HeadPowder’s solutions are designed to be durable and low-maintenance, ensuring long-term reliability and cost-effectiveness for clients.
Applications and Case Studies
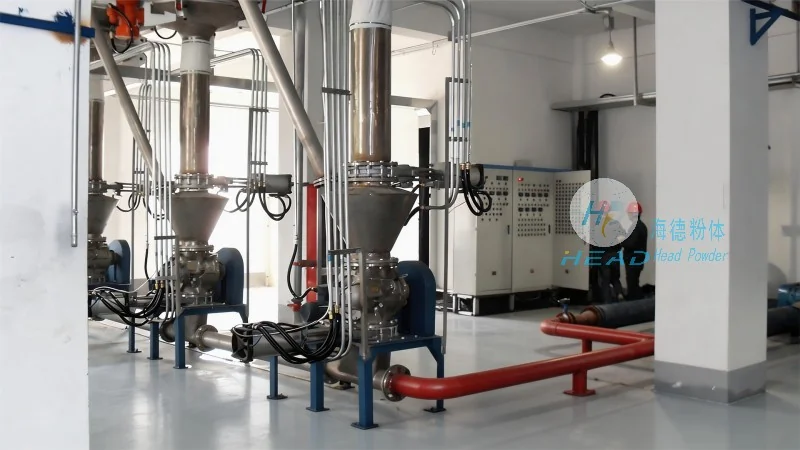
The effectiveness of airflow transport for anhydrous sodium sulfate has been demonstrated in various industrial settings. For example, in glass manufacturing plants, HeadPowder’s systems have enabled seamless transfer of sodium sulfate from storage silos to production lines, improving production throughput and reducing material waste. Similarly, in detergent production facilities, the technology has been used to transport the chemical to mixing and packaging areas, ensuring a consistent supply while maintaining strict hygiene standards. These applications highlight the versatility and adaptability of HeadPowder’s airflow transport solutions across different industries.
Conclusion and Future Outlook
As industries continue to prioritize efficiency and sustainability, airflow transport systems for anhydrous sodium sulfate remain a critical component of modern material handling strategies. HeadPowder Engineering Co., Ltd., with its expertise and commitment to innovation, provides tailored solutions that address the unique challenges of handling this chemical. By leveraging advanced technology and a customer-centric approach, HeadPowder helps clients achieve optimal performance, safety, and environmental compliance in their material transport operations. For businesses seeking to enhance their anhydrous sodium sulfate handling processes, HeadPowder’s airflow transport solutions offer a reliable and forward-thinking approach to material management.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu