Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Efficient and environmentally friendly material transport solutions are increasingly critical in modern industrial operations, particularly for handling bulk materials like corn kernels. The traditional methods of conveying such materials often face challenges related to operational efficiency, environmental impact, and maintenance costs. In response to these challenges, advanced pneumatic conveying systems have emerged as a superior alternative, offering a seamless blend of performance and sustainability. This article explores the benefits and applications of corn kernel pneumatic conveying, highlighting how it addresses the evolving needs of the agricultural and processing industries.
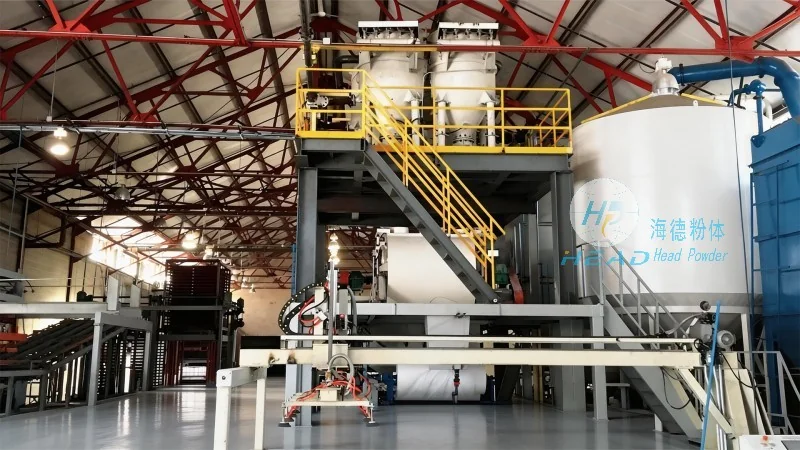
Introduction to Pneumatic Conveying for Corn Kernels
When it comes to transporting corn kernels, the choice of conveying system can significantly impact the overall productivity and sustainability of a facility. Conventional methods such as belt conveyors or bucket elevators may struggle with material handling efficiency, especially when dealing with high volumes or sensitive products. Pneumatic conveying, on the other hand, utilizes air to transport particles through a pipeline system, providing a more controlled and efficient approach. This technology not only enhances the speed and reliability of material transport but also minimizes the environmental footprint associated with traditional methods.
About HeadPowder: A Leader in Material Handling Solutions
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., is a trusted provider of innovative material handling solutions tailored to the unique demands of the agricultural and industrial sectors. With operations based in Shandong, China, HeadPowder leverages decades of expertise to design, manufacture, and implement advanced pneumatic conveying systems. The company’s commitment to quality, efficiency, and environmental responsibility has established it as a leading name in the industry, serving clients worldwide with customized solutions that meet their specific operational requirements.
The Advantages of Corn Kernel Pneumatic Conveying
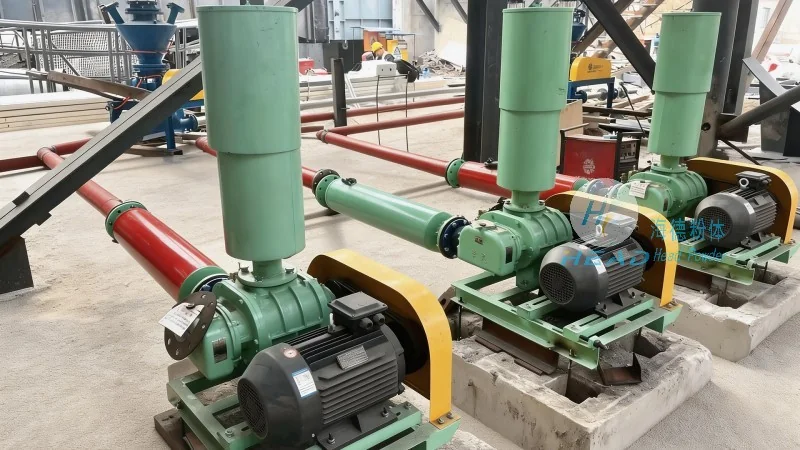
For corn kernel processing facilities, pneumatic conveying offers several key advantages that set it apart from conventional methods. Firstly, it significantly improves operational efficiency by reducing downtime and increasing throughput. The system’s ability to handle high volumes of material with minimal manual intervention streamlines production processes, allowing facilities to meet growing market demands. Secondly, pneumatic conveying is highly effective in maintaining product quality. Unlike mechanical systems that may cause abrasion or breakage, the air-based transport minimizes particle damage, preserving the integrity of the corn kernels. This is particularly important for applications where the quality of the final product is paramount, such as in food processing or animal feed production.
Furthermore, the environmental benefits of pneumatic conveying are substantial. By eliminating the need for open-air transport or manual handling, the system reduces dust emissions and minimizes the risk of contamination. This not only complies with stringent environmental regulations but also contributes to a safer working environment for personnel. Additionally, the energy efficiency of modern pneumatic conveying systems further enhances their appeal, as they consume less power compared to traditional methods while delivering superior performance.
Technical Aspects of the Pneumatic Conveying System
The core of a corn kernel pneumatic conveying system lies in its components and operational principles. The system typically consists of a hopper for material storage, a blower or compressor to generate the air flow, a pipeline network to transport the material, and a receiver or discharge point for the final product. The design of the system is tailored to the specific characteristics of corn kernels, such as their size, density, and moisture content, ensuring optimal performance. For example, the selection of the blower’s capacity and the pipeline’s diameter is critical to maintaining the right air velocity for efficient transport without causing excessive pressure drops or material degradation.
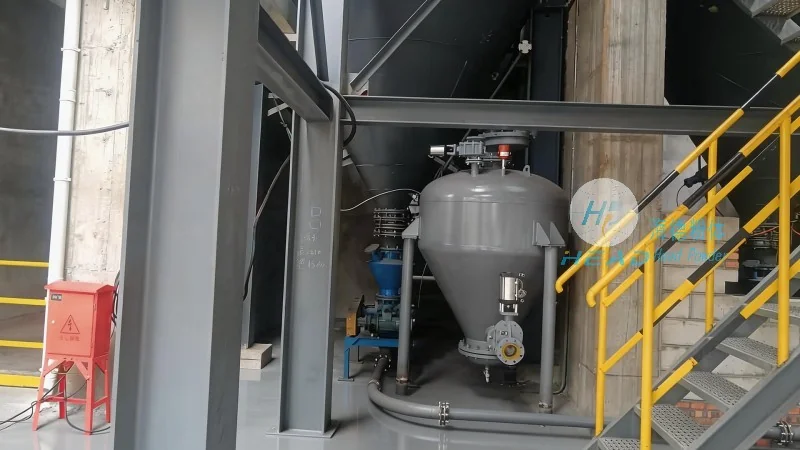
HeadPowder’s engineers employ advanced engineering techniques to optimize the system’s performance. They consider factors such as the material’s flowability, the required conveying distance, and the desired discharge rate to design a system that meets the client’s exact needs. The use of high-quality materials for the pipeline and components ensures durability and long-term reliability, reducing maintenance costs and extending the system’s lifespan. Moreover, the integration of automation and control systems allows for real-time monitoring and adjustment, further enhancing the system’s efficiency and adaptability.
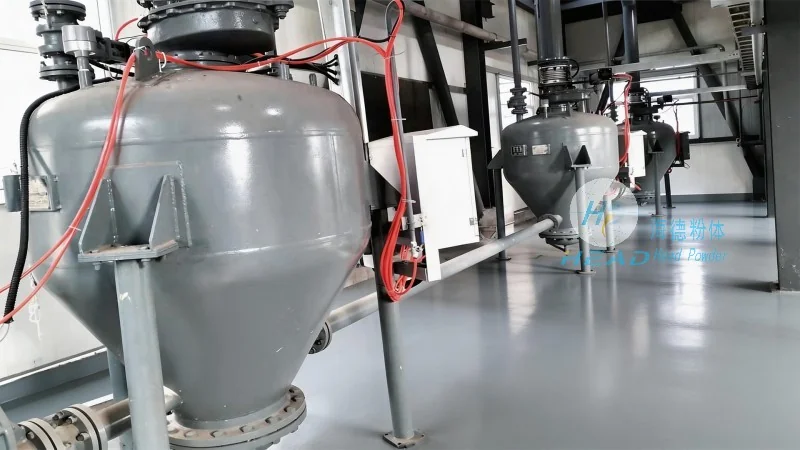
Applications and Case Studies
Corn kernel pneumatic conveying is widely used in various applications across the agricultural and food processing industries. In grain storage facilities, the system efficiently transports corn kernels from storage silos to processing plants, ensuring a continuous supply of raw material. In food processing plants, it is used to move corn kernels to milling or grinding operations, where the material is processed into flour, cornmeal, or other products. The system’s versatility also makes it suitable for animal feed production, where it can transport corn kernels to feed mills, ensuring consistent and high-quality feed production.
HeadPowder has successfully implemented numerous pneumatic conveying systems for clients in the corn processing sector. For instance, a major corn milling company in the United States partnered with HeadPowder to upgrade its material handling system. The new pneumatic conveying system increased the facility’s throughput by 30% while reducing energy consumption by 20%. The system’s ability to handle high volumes of corn kernels without causing product damage also improved the quality of the final flour, leading to higher customer satisfaction. Another case study involves a feed mill in China, where HeadPowder’s system helped the facility achieve a 25% reduction in dust emissions, meeting the local environmental regulations and enhancing workplace safety.
Conclusion: The Future of Corn Kernel Transport
As the demand for efficient and sustainable material transport solutions continues to grow, corn kernel pneumatic conveying stands out as a reliable and advanced technology. By combining operational efficiency with environmental responsibility, this system addresses the key challenges faced by modern corn processing facilities. HeadPowder, with its expertise and commitment to innovation, remains at the forefront of providing tailored solutions that meet the evolving needs of the industry. For facilities looking to enhance their material handling capabilities while reducing their environmental impact, pneumatic conveying offers a compelling and effective solution.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu