Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Ammonium bicarbonate, a widely used chemical in various industrial applications, requires reliable and efficient material handling solutions to ensure smooth production processes. Traditional methods often face challenges such as dust contamination, material loss, and operational inefficiencies. Pneumatic conveying has emerged as a superior alternative, offering a clean, safe, and eco-friendly approach to transporting this critical substance. This article explores the benefits of ammonium bicarbonate pneumatic conveying and highlights the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for this demanding application.
Understanding Ammonium Bicarbonate and Its Handling Challenges
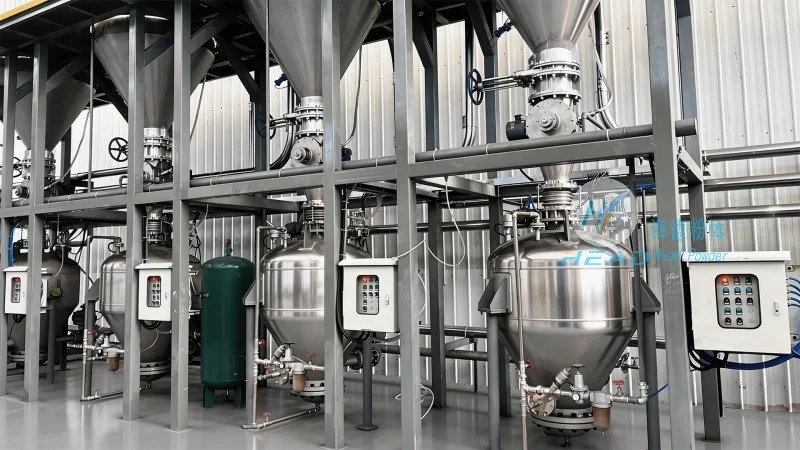
Ammonium bicarbonate (NH₄HCO₃) is a white crystalline powder commonly utilized in the food, pharmaceutical, and chemical industries. Its properties, including hygroscopic nature and potential for dust generation, make conventional handling methods like manual shoveling or bucket elevators impractical and hazardous. These traditional approaches not only lead to product degradation but also pose health risks due to dust inhalation and environmental pollution. The need for a more advanced, automated system has driven the adoption of pneumatic conveying technology, which addresses these challenges effectively.
Pneumatic Conveying Technology: A Superior Solution for Ammonium Bicarbonate
Pneumatic conveying systems utilize air or gas to transport bulk materials through a closed pipeline network. This method eliminates the need for manual handling, reduces dust exposure, and minimizes material spillage. For ammonium bicarbonate, which is sensitive to moisture and temperature fluctuations, the closed system of pneumatic conveying provides a controlled environment that preserves product quality. The technology is available in various configurations, including dilute phase and dense phase systems, allowing customization based on the specific requirements of the application.
Key Advantages of Ammonium Bicarbonate Pneumatic Conveying
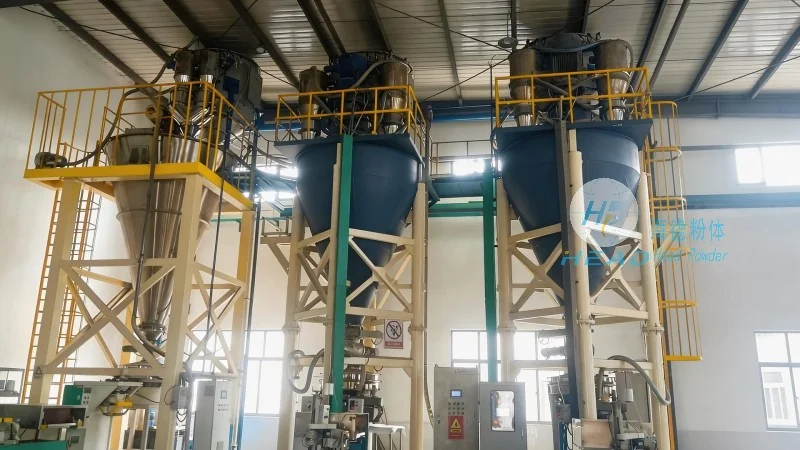
Implementing pneumatic conveying for ammonium bicarbonate offers several significant advantages. Firstly, it enhances operational efficiency by automating the material transport process, reducing labor costs and increasing production throughput. Secondly, the closed system ensures environmental compliance by preventing dust emissions and minimizing the risk of product contamination. This is particularly important for industries where product purity is critical, such as food and pharmaceutical manufacturing. Additionally, the system reduces maintenance costs compared to traditional equipment, as it has fewer moving parts and lower wear and tear.
HeadPowder Engineering: Expertise in Ammonium Bicarbonate Pneumatic Conveying
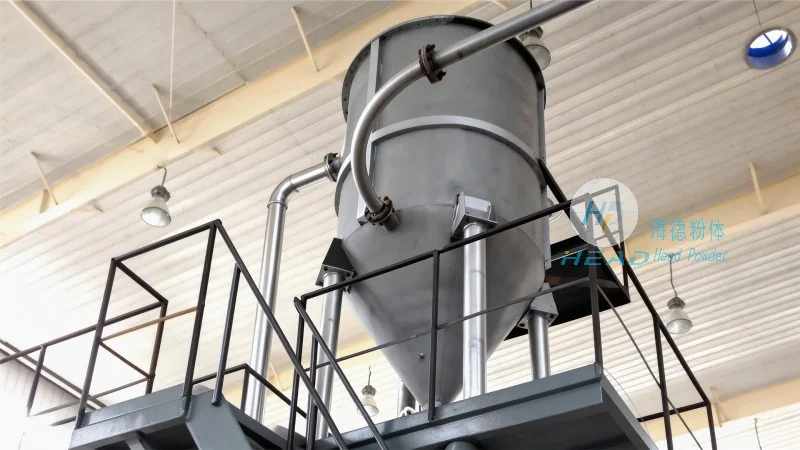
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of customized material handling solutions. With years of experience in the industry, HeadPowder specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of ammonium bicarbonate applications. The company’s team of engineers leverages advanced technology and industry best practices to develop solutions that optimize efficiency, ensure product integrity, and meet environmental standards. HeadPowder’s commitment to quality and customer satisfaction has made it a trusted partner for businesses seeking reliable and sustainable material handling solutions.
Tailored Solutions for Diverse Industrial Needs
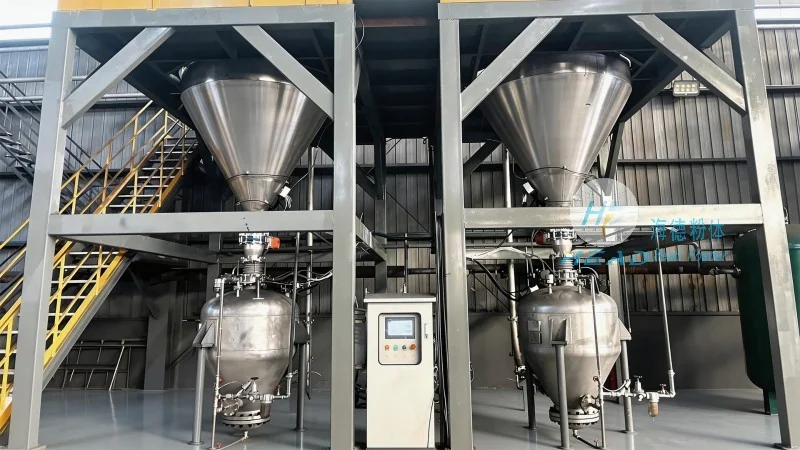
HeadPowder understands that each industrial facility has distinct requirements when it comes to ammonium bicarbonate handling. The company offers a range of pneumatic conveying solutions, from simple dilute phase systems for short-distance transport to complex dense phase systems for high-capacity and precise delivery. These solutions can be integrated with existing production lines or designed as standalone systems, ensuring seamless operation and minimal disruption to current processes. HeadPowder’s approach involves thorough consultation with clients to assess their specific needs, including material flow rates, distance, and environmental regulations, before developing a customized solution.
Ensuring Product Quality and Environmental Compliance
For ammonium bicarbonate, maintaining product quality and adhering to environmental regulations is paramount. HeadPowder’s pneumatic conveying systems are engineered to minimize product degradation, prevent moisture absorption, and reduce dust generation. The closed pipeline design ensures that the material remains in a controlled environment throughout the conveying process, preserving its purity and effectiveness. Additionally, the systems are designed to meet or exceed local and international environmental standards, reducing the risk of regulatory penalties and enhancing the company’s sustainability profile.
Conclusion: The Future of Ammonium Bicarbonate Handling
As industries continue to prioritize efficiency, safety, and environmental responsibility, pneumatic conveying has become the preferred method for handling ammonium bicarbonate. Shandong HeadPowder Engineering Co., Ltd. stands at the forefront of this technology, providing innovative and reliable solutions that meet the evolving needs of modern manufacturing. By leveraging their expertise and commitment to quality, HeadPowder helps businesses optimize their material handling processes, reduce costs, and enhance overall operational performance. For companies seeking a sustainable and efficient solution for ammonium bicarbonate transport, HeadPowder offers a comprehensive range of services and products designed to deliver exceptional results.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu