Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Cement raw material pneumatic conveying is a critical technology in the cement industry, offering a reliable and efficient method for transporting bulk materials. This article explores the advantages of pneumatic conveying systems for cement raw materials, highlighting their role in enhancing operational efficiency and environmental sustainability.
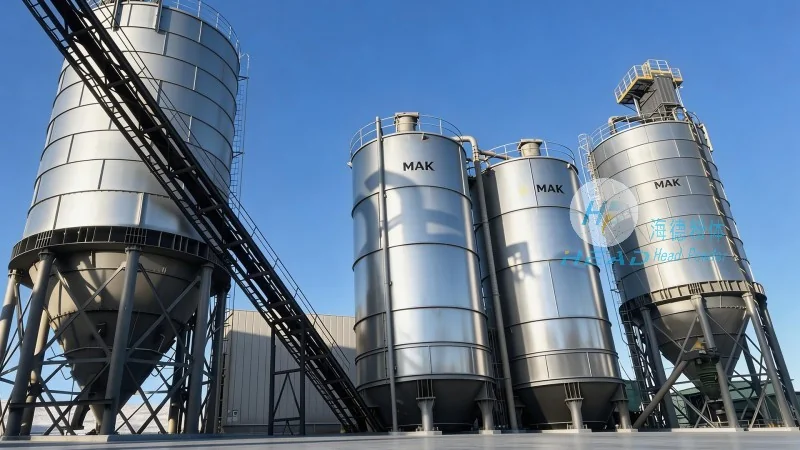
Introduction to Pneumatic Conveying in Cement Production
Pneumatic conveying systems utilize air or gas to transport bulk materials like cement raw materials, clinker, and additives through pipelines. Unlike traditional mechanical conveying methods, such as belt conveyors or bucket elevators, pneumatic conveying offers several advantages, including reduced equipment complexity, lower maintenance costs, and improved safety. The technology is particularly well-suited for handling fine powders and granular materials, which are common in cement production processes.
HeadPowder: A Leading Provider of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of advanced pneumatic conveying equipment in China. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner for cement plants and other industrial facilities seeking reliable material handling systems. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies tailored to the specific needs of the cement industry.
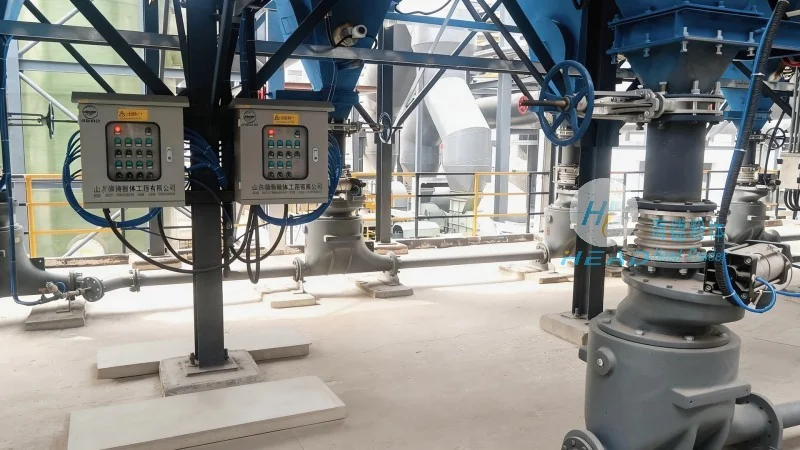
Key Features of Pneumatic Conveying Systems for Cement Raw Materials
The pneumatic conveying systems offered by HeadPowder are designed to address the unique challenges of cement raw material transport. These systems are equipped with high-efficiency air compressors, advanced control systems, and durable pipeline components that ensure consistent and reliable material flow. The technology supports both positive and negative pressure conveying modes, allowing flexibility in system design and operation. Additionally, the systems are engineered to minimize dust emissions and noise pollution, contributing to a cleaner and safer working environment.
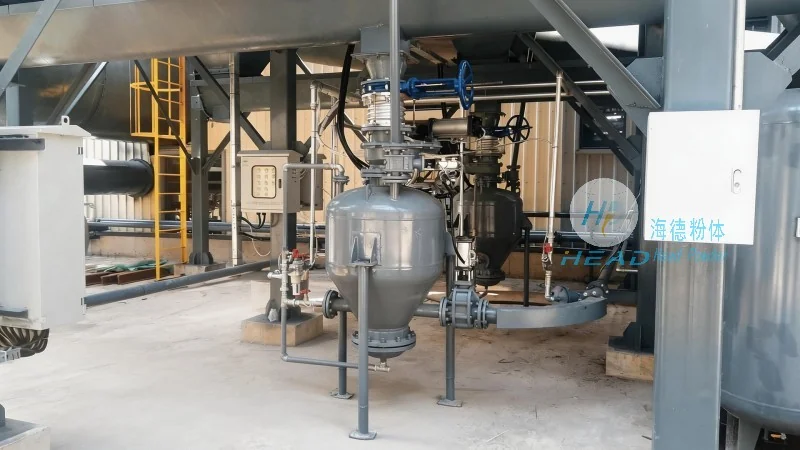
Efficiency and Environmental Benefits
One of the primary advantages of pneumatic conveying for cement raw materials is its ability to significantly improve operational efficiency. By eliminating the need for multiple transfer points and reducing material handling time, these systems enhance overall production throughput. Furthermore, the technology promotes environmental sustainability by reducing energy consumption compared to traditional mechanical conveying methods. The closed-loop design of the systems minimizes material loss and dust dispersion, aligning with modern environmental regulations and corporate sustainability goals.
Technical Advantages and Customization Options
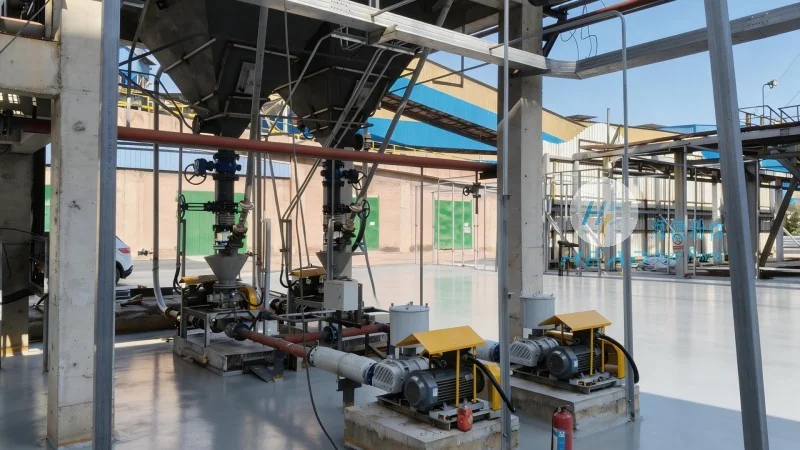
HeadPowder's pneumatic conveying solutions are built on robust engineering principles, ensuring long-term reliability and low operational costs. The company offers a range of customization options to suit different plant sizes and material characteristics. This includes adjustable conveying velocities, variable pipeline configurations, and integrated dust collection systems. The systems are also equipped with advanced monitoring and diagnostic tools, enabling real-time performance tracking and proactive maintenance. Such features help cement plants optimize their operations and extend the lifespan of the conveying equipment.
Application Scenarios and Industry Impact
Pneumatic conveying systems are widely used in various stages of cement production, including raw material storage, grinding, and clinker handling. In raw material storage, the systems efficiently transport limestone, clay, and other raw materials from silos to grinding mills. During the grinding process, they facilitate the transport of fine powders between grinding units and storage silos. For clinker handling, pneumatic conveying offers a safe and efficient method to move clinker from the kiln to the cement packing or storage areas. The consistent performance of these systems ensures stable production processes and reduces downtime, contributing to higher overall plant productivity.
Conclusion: The Future of Cement Raw Material Handling
As the cement industry continues to evolve, the demand for efficient and environmentally friendly material handling solutions remains high. Pneumatic conveying systems, particularly those provided by companies like HeadPowder, play a pivotal role in meeting these demands. By combining advanced technology with practical design, these systems offer cement plants a reliable pathway to enhance operational efficiency, reduce costs, and minimize environmental impact. With a strong presence in China and a commitment to innovation, HeadPowder is well-positioned to support the growth and sustainability of the cement industry through its cutting-edge pneumatic conveying solutions.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu