Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
When it comes to the efficient and reliable transport of purified ash, selecting the right conveying method is crucial for industrial operations. Purified ash, often a byproduct of industrial processes such as power generation or chemical manufacturing, requires specialized handling to ensure safety, efficiency, and environmental compliance. Among the various options available, pneumatic conveying stands out as a preferred solution due to its unique advantages and features. This article explores the different methods of purified ash conveyance and highlights the benefits of using pneumatic systems, with insights from Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
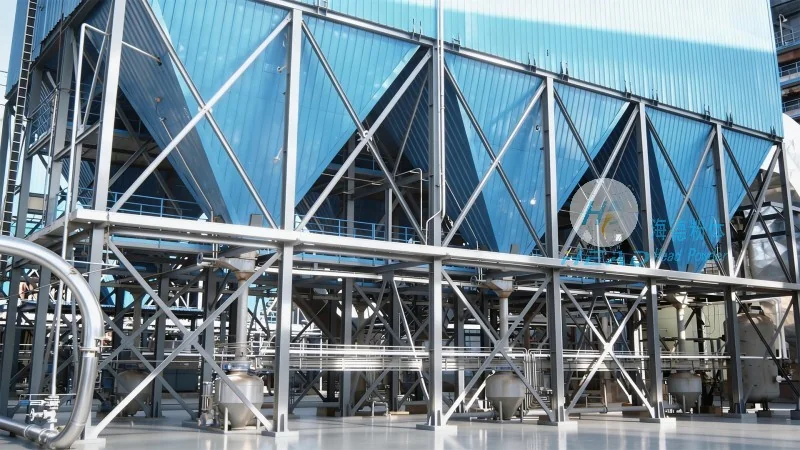
Understanding Purified Ash and Its Conveying Requirements
Purified ash, also known as fly ash or bottom ash after processing, is a fine particulate material that poses challenges in traditional bulk material handling. Its properties, including particle size, moisture content, and chemical composition, influence the choice of conveying technology. Unlike bulk materials like coal or cement, purified ash demands systems that can handle fine particles without clogging, maintain consistent flow rates, and minimize dust emissions. These requirements have led to the development of specialized conveying methods, with pneumatic conveying emerging as a robust solution.
Common Conveying Methods for Purified Ash
Several conventional and modern methods are employed for transporting purified ash, each with its own set of applications and limitations. The primary options include:
Gravity Conveying: This method relies on the natural force of gravity to move ash from one point to another. It typically involves inclined chutes or hoppers that allow the material to flow down due to its weight. While simple and low-cost, gravity conveying is limited by the slope of the path and is not suitable for long distances or vertical lifts. It also requires careful design to prevent material buildup and ensure smooth flow.
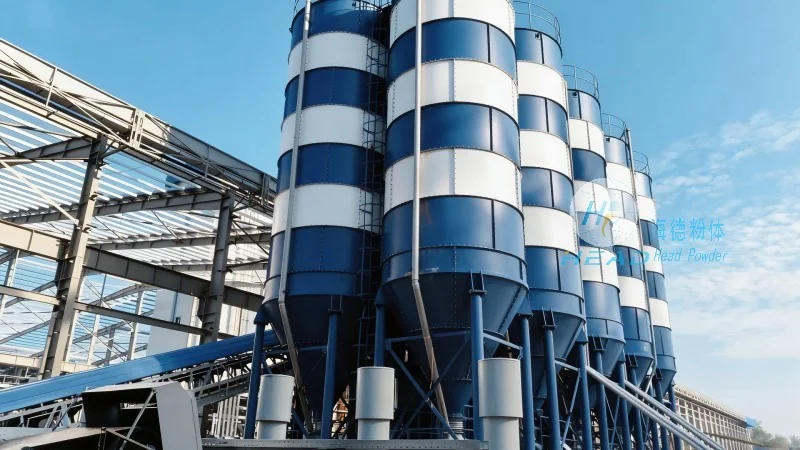
Pneumatic Conveying: As an alternative to gravity, pneumatic systems use compressed air or gas to transport ash through a pipeline. This method is highly versatile and can handle both fine and coarse particles, making it ideal for purified ash. It offers the ability to move materials over long distances, including vertical lifts, and can be integrated with other processing equipment.
Mechanical Conveying: Mechanical systems, such as belt conveyors, screw conveyors, and bucket elevators, are widely used in industrial settings. These methods are effective for transporting bulk materials but may face challenges with fine particulate materials like purified ash. Issues like clogging, material degradation, and high maintenance costs are common with mechanical conveyors, especially when dealing with abrasive or sticky ash.
Hydraulic Conveying: This method uses water or other liquids to transport ash through pipelines. It is suitable for wet ash or materials that require a slurry form. However, hydraulic systems are less common for purified ash due to the potential for corrosion, higher energy consumption, and the need for additional equipment to separate water from the ash.
Pneumatic Conveying: Advantages and Features for Purified Ash
Among the various conveying methods, pneumatic conveying has gained significant traction in the handling of purified ash. The advantages of pneumatic systems, as highlighted by Shandong HeadPowder Engineering Co., Ltd., include:
Efficient and Flexible Transport: Pneumatic systems can transport purified ash over long distances, including horizontal and vertical routes, with minimal loss of material. The ability to adjust air pressure and flow rates allows for precise control over the conveying process, ensuring consistent delivery to processing units or storage facilities.
Low Maintenance and Reduced Downtime: Unlike mechanical conveyors that require regular maintenance and part replacement, pneumatic systems have fewer moving parts. This results in lower maintenance costs and reduced downtime, enhancing overall operational efficiency. The absence of mechanical components also minimizes the risk of material degradation or contamination.
Environmental Benefits: Pneumatic conveying helps in maintaining a clean and dust-free environment by enclosing the material within a pipeline. This reduces dust emissions and improves workplace safety, which is critical in industrial settings where purified ash handling occurs. The system also minimizes the risk of material spillage, contributing to better environmental compliance.
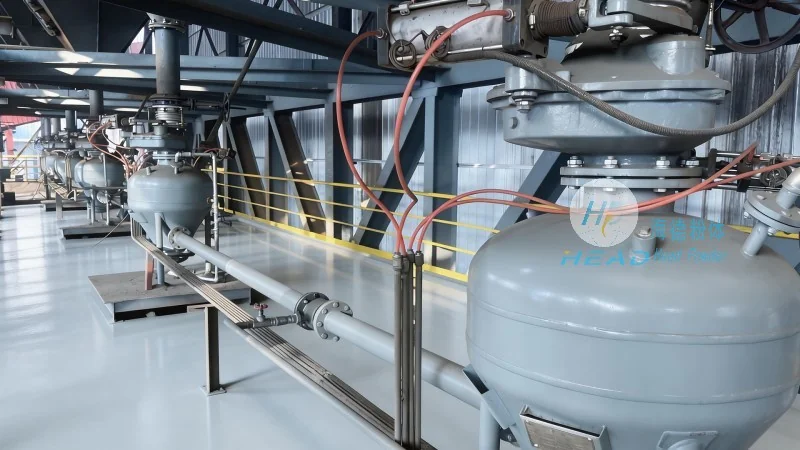
Scalability and Integration: Pneumatic systems can be easily scaled to accommodate varying production volumes and integrated with other industrial processes. Whether for small-scale operations or large-scale power plants, the flexibility of pneumatic conveying allows for customized solutions that meet specific operational needs. This adaptability makes it a preferred choice for industries dealing with purified ash.
Energy Efficiency: Modern pneumatic conveying systems are designed to be energy-efficient, utilizing compressed air in a controlled manner. The use of optimized air flow and pressure settings reduces energy consumption compared to traditional mechanical methods. This not only lowers operational costs but also aligns with sustainability goals in industrial operations.
Key Features of Pneumatic Conveying for Purified Ash
In addition to the advantages mentioned above, pneumatic conveying systems for purified ash offer several key features that enhance their performance and reliability:
Positive Displacement and Dilute Phase Conveying: Pneumatic systems can operate in both positive displacement (high-pressure) and dilute phase (low-pressure) modes. Positive displacement is suitable for short distances or high-density materials, while dilute phase is ideal for long-distance and fine particle transport. For purified ash, dilute phase systems are often preferred due to their ability to handle fine particles without clogging.
Material Handling Capabilities: These systems can handle a wide range of ash types, including fly ash, bottom ash, and blended ash. The flexibility in material handling allows for the transport of ash with varying moisture content and particle sizes, ensuring compatibility with different industrial applications.
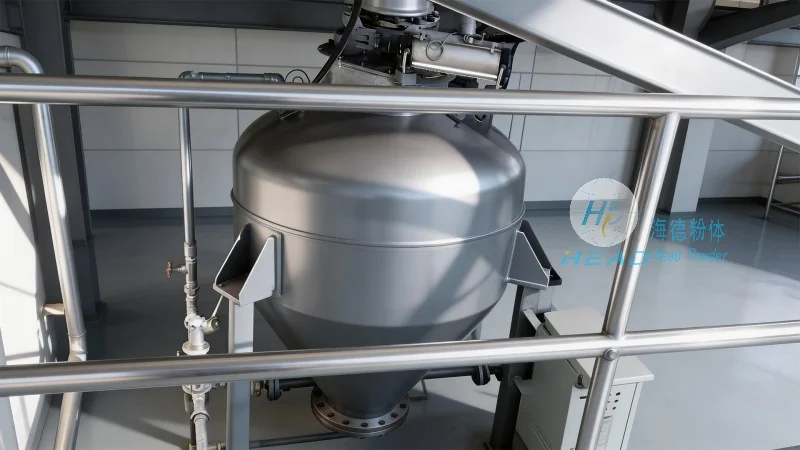
Control and Monitoring Systems: Advanced pneumatic conveying systems are equipped with sensors and control panels that monitor pressure, flow rate, and material level in real-time. This allows operators to adjust the system parameters dynamically, ensuring optimal performance and preventing issues such as clogging or overloading.
Customizable Design: Shandong HeadPowder Engineering Co., Ltd. offers customized pneumatic conveying solutions tailored to the specific requirements of each client. From pipeline layout to air compressor selection, the company provides comprehensive design and engineering services to ensure the system meets operational and safety standards.
Conclusion: Choosing the Right Conveying Method for Purified Ash
When selecting a conveying method for purified ash, it is essential to consider the specific requirements of the industrial process, including material properties, distance, and operational constraints. While gravity and mechanical methods have their applications, pneumatic conveying offers superior advantages in terms of efficiency, flexibility, and environmental impact. With its ability to handle fine particles, minimize maintenance, and provide scalable solutions, pneumatic systems are increasingly becoming the preferred choice for industries dealing with purified ash.
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pneumatic conveying solutions for purified ash, leveraging years of experience and expertise in the field. The company's commitment to quality, innovation, and customer satisfaction ensures that clients receive tailored systems that enhance operational efficiency and meet industry standards. Whether for new installations or system upgrades, HeadPowder offers reliable and effective solutions to meet the conveying needs of purified ash in various industrial applications.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu