Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Sodium bicarbonate, also known as baking soda, is a versatile chemical widely utilized in industrial, commercial, and even household applications. Its effective delivery is critical for maintaining consistent performance and safety across various processes. This article provides a detailed comparison of common sodium bicarbonate delivery methods, exploring the technologies and considerations that influence the choice of system for different applications.
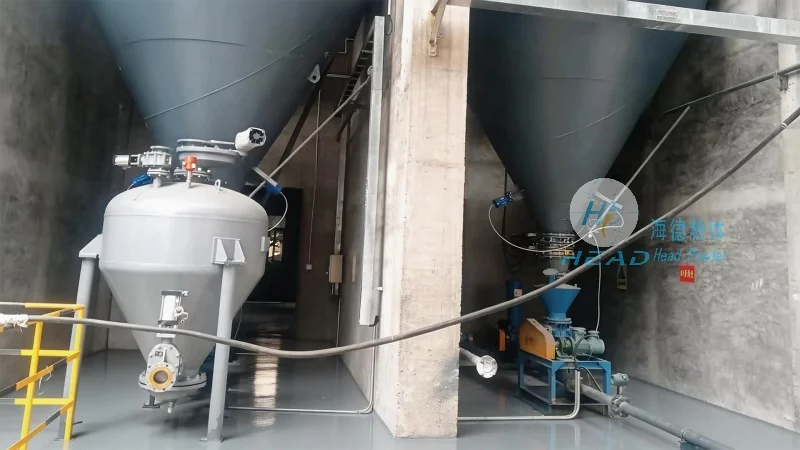
1. Pneumatic Conveying Systems
Pneumatic conveying is a prevalent method for transporting sodium bicarbonate, particularly in bulk operations. This technique leverages compressed air or other gases to move the material through a pipeline. Two primary types exist: dilute-phase and dense-phase pneumatic conveying. Dilute-phase systems are suitable for lighter materials and longer transport distances, while dense-phase systems offer superior control and are ideal for handling more abrasive or sensitive products. The selection of a pneumatic conveying system depends on factors such as the material's density, flow rate requirements, and the distance between the source and destination. These systems are often preferred in industries like food processing, pharmaceuticals, and chemical manufacturing where hygiene and product integrity are paramount. For example, in food production, pneumatic conveying can be used to transport sodium bicarbonate from storage silos to processing lines without direct human contact, ensuring food safety standards are met.
2. Mechanical Conveying Equipment
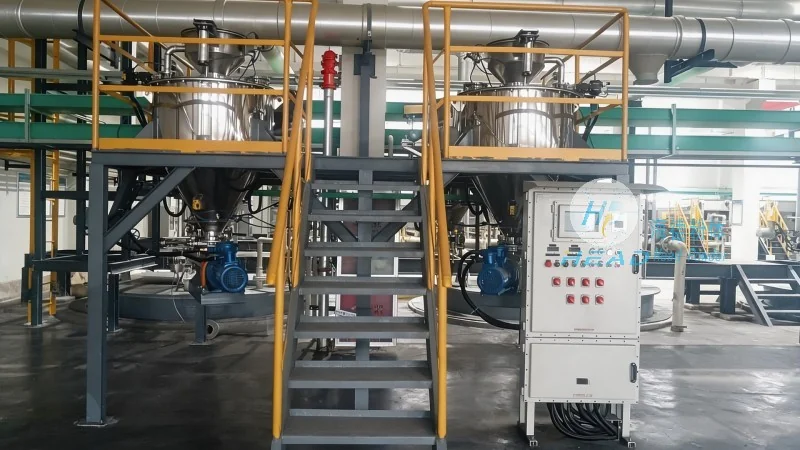
Mechanical conveying methods, including screw conveyors, belt conveyors, and bucket elevators, are widely adopted for sodium bicarbonate delivery. Screw conveyors are particularly effective for moving dry powders in a controlled manner, minimizing segregation and loss. They are commonly used in storage and handling operations where a continuous flow is required. Belt conveyors are suitable for larger volumes and can handle bulk loads efficiently, making them ideal for material transfer over medium distances. Bucket elevators are used for vertical transport, providing a reliable solution for moving material from lower to higher levels. These systems are often chosen when the material needs to be transported over short to medium distances and where a consistent flow rate is essential. In industrial settings, mechanical conveyors are often integrated with storage silos and processing equipment to create a seamless material handling workflow.
3. Metering and Dosing Pumps
For applications requiring precise control over the amount of sodium bicarbonate delivered, metering and dosing pumps are indispensable. These devices are commonly employed in chemical processing, water treatment, and food production to ensure accurate dosing of the substance. Positive displacement pumps, such as diaphragm or plunger pumps, are ideal for handling viscous or shear-sensitive materials, guaranteeing accurate flow rates. Peristaltic pumps offer flexibility with various fluid viscosities and the ability to handle solids in suspension, making them suitable for slurry applications. The selection of a metering pump depends on the required flow rate, pressure, and the specific characteristics of the sodium bicarbonate solution or slurry being processed. These pumps are crucial for maintaining process consistency and meeting regulatory requirements in industries where precise chemical addition is critical. For instance, in water treatment plants, dosing pumps are used to add sodium bicarbonate to adjust pH levels, and the accuracy of these pumps directly impacts water quality and treatment efficiency.

About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for material handling and processing. With decades of experience in the industry, the company offers a range of equipment tailored to the unique needs of sodium bicarbonate delivery. Their products are designed to ensure efficiency, reliability, and safety, meeting the demands of various industrial applications. HeadPowder Engineering Co., Ltd. is committed to delivering high-quality solutions that enhance operational performance and support sustainable practices. The company's expertise in engineering and manufacturing ensures that clients receive customized solutions that address specific challenges in sodium bicarbonate handling and processing. Whether for bulk transport, precise dosing, or integrated system solutions, HeadPowder Engineering Co., Ltd. provides comprehensive support from design to installation and maintenance, helping businesses optimize their sodium bicarbonate delivery processes.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu