Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
For industries dealing with bulk materials like flour and grains, selecting the right conveying system is crucial for efficiency, cost-effectiveness, and product integrity. This article provides a detailed comparison of common conveying methods used in the milling and processing sectors, focusing on their advantages and disadvantages to help businesses make informed decisions.
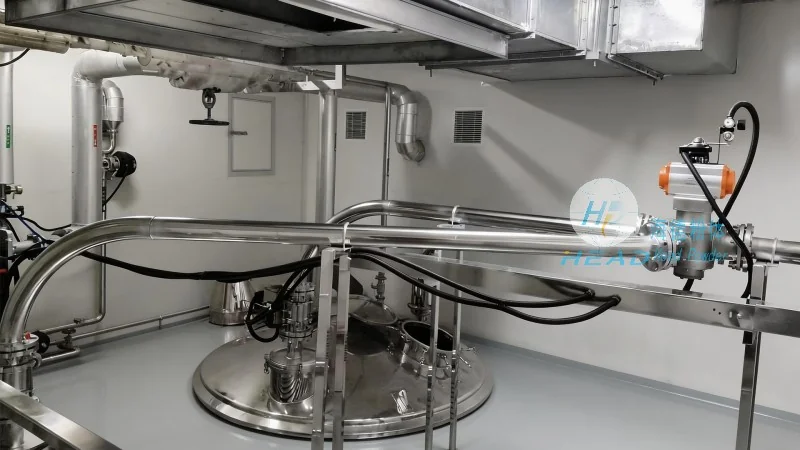
1. Screw Conveyors: The Workhorse of Bulk Material Handling
Screw conveyors, also known as auger conveyors, are among the most widely used systems for transporting dry, free-flowing materials such as flour and grains. These systems consist of a rotating helical screw inside a tube or trough, which moves material from one point to another through gravitational force and the screw's rotation. The primary advantage of screw conveyors is their simplicity and low cost, making them an attractive option for many applications. They are also relatively easy to install and maintain, with minimal moving parts that reduce the risk of mechanical failure. Additionally, screw conveyors can handle a wide range of materials, including powders and granules, without the need for additional equipment like hoppers or feeders. However, their limitations become apparent when dealing with sticky or abrasive materials, as the screw and trough can experience significant wear and tear. Moreover, screw conveyors are not suitable for vertical lifting over large heights, as the power required increases dramatically with the vertical distance. The design also restricts the flow rate and can lead to material degradation if the speed is too high, potentially affecting the quality of the final product.
2. Belt Conveyors: High-Capacity and Versatile Solutions
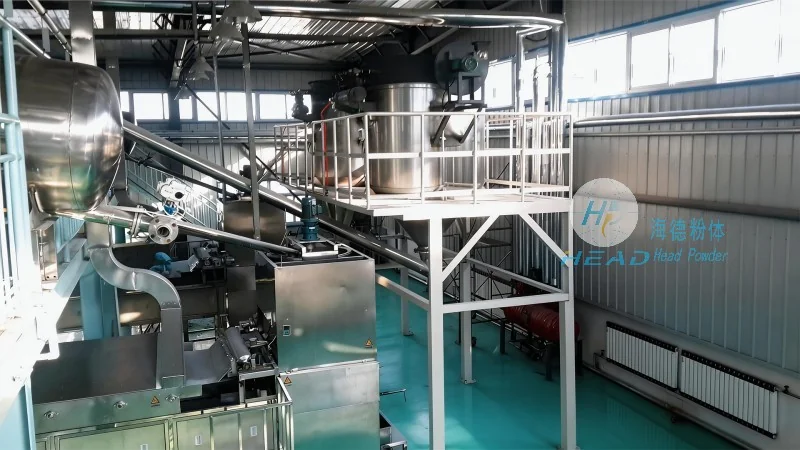
Belt conveyors are another popular choice for conveying flour and grains, particularly in applications requiring high throughput and long-distance transport. These systems use a continuous belt looped over rollers, with the material placed on the belt and carried to the destination. The main advantage of belt conveyors is their ability to handle large volumes of material at high speeds, making them ideal for large-scale operations. They are also versatile, as they can be adapted for horizontal, inclined, or even vertical transport with the use of idlers and incline angles. Belt conveyors are relatively low-maintenance compared to other systems, as the primary wear parts are the rollers and the belt itself, which can be easily replaced. However, their design has some drawbacks. For instance, they require a significant amount of space for installation, especially for long-distance runs. Additionally, belt conveyors are susceptible to material spillage and contamination if the belt is not properly sealed or if the load is uneven. The belt also needs to be cleaned regularly to prevent buildup of flour or grain, which can affect performance and hygiene. Furthermore, belt conveyors are not suitable for conveying sticky or heavy materials, as the belt may slip or become damaged under excessive load.
3. Pneumatic Conveying Systems: The Flexible and Clean Option
Pneumatic conveying systems use air or other gases to transport dry materials like flour and grains through a network of pipes. These systems are often categorized into two types: pressure and vacuum. Pressure systems use compressed air to push the material forward, while vacuum systems use suction to draw the material into the system. The primary advantage of pneumatic conveying is its flexibility, as it can be easily integrated into existing facilities and adapted to various layouts. It also offers a clean and hygienic method of transport, as the material is contained within the pipes, reducing the risk of contamination and dust exposure. Pneumatic systems are particularly suitable for conveying materials that are sensitive to moisture or temperature changes, as the air can be filtered and conditioned to maintain optimal conditions. However, pneumatic conveying has several limitations. The most significant drawback is the high energy consumption, as it requires significant air pressure or vacuum to move the material. This can lead to higher operational costs compared to other systems. Additionally, the system can be prone to blockages if the material is too fine or has high moisture content, which may require regular maintenance and cleaning. The design also limits the distance over which material can be conveyed, as the pressure or vacuum drops with distance, potentially affecting the efficiency of long runs. Furthermore, the system may not be suitable for heavy or abrasive materials, as the pipes and components can experience wear and tear from the material's impact.
4. Bucket Elevators: Efficient Vertical Transport Solutions
Bucket elevators are specialized conveying systems designed for vertical transport of bulk materials, including flour and grains. These systems consist of a continuous chain with buckets attached, which moves up and down inside a vertical casing. The material is loaded into the buckets at the bottom and discharged at the top, allowing for efficient vertical lifting. The main advantage of bucket elevators is their high efficiency in vertical transport, as they can move material over large vertical distances with minimal power consumption compared to other vertical systems. They are also relatively compact, requiring less floor space than other vertical conveying methods. Bucket elevators are ideal for applications where vertical lifting is necessary, such as in flour mills or grain processing plants. However, their design has some limitations. The system is relatively complex, with more moving parts compared to other systems, which increases the risk of mechanical failure and maintenance requirements. The buckets and chain can also experience significant wear and tear, especially when handling abrasive or sticky materials. Additionally, bucket elevators are not suitable for conveying materials that are too fine or have high moisture content, as the buckets may not be able to effectively hold the material, leading to spillage or reduced capacity. The system also requires regular inspection and maintenance to ensure proper operation and prevent material buildup or blockages.
5. Chain and Flight Conveyors: Robust and Durable Solutions
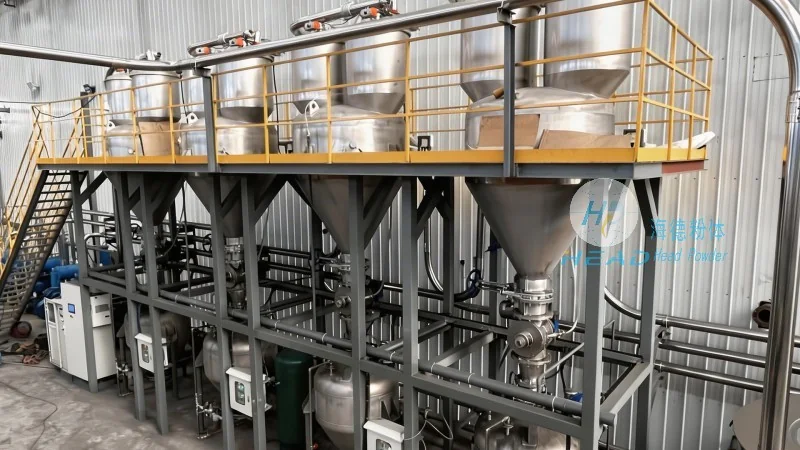
Chain and flight conveyors are heavy-duty systems designed for transporting bulk materials like flour and grains in harsh environments or high-traffic applications. These systems use a chain with flights (flights are the paddles or blades attached to the chain) that move material along a trough or belt. The primary advantage of chain and flight conveyors is their durability and ability to handle heavy loads, making them suitable for industrial settings with high wear and tear. They are also relatively low-maintenance, as the main components are the chain and flights, which can be easily replaced. Chain and flight conveyors are ideal for applications where the material is abrasive or sticky, as the flights can effectively move the material without causing excessive wear. However, their design has some drawbacks. The system is relatively large and bulky, requiring significant space for installation. Additionally, chain and flight conveyors are not suitable for conveying fine powders or materials that are prone to caking, as the flights may not be able to effectively transport the material. The system also requires regular cleaning to prevent material buildup and maintain efficiency. Furthermore, the chain and flights can experience significant wear and tear, especially when handling heavy or abrasive materials, which may require more frequent maintenance and replacement.
6. Conclusion: Choosing the Right Conveying System for Your Needs
Selecting the appropriate conveying system for flour and grain handling depends on several factors, including the material properties, required throughput, distance, and operational environment. Each system has its own advantages and disadvantages, and the best choice will vary based on the specific application. For example, screw conveyors are ideal for simple, low-cost applications with moderate throughput, while belt conveyors are better suited for high-volume, long-distance transport. Pneumatic systems offer flexibility and cleanliness but at a higher energy cost, and bucket elevators are efficient for vertical lifting. Chain and flight conveyors provide durability for harsh environments. It is essential to consider the material's characteristics, such as its flowability, moisture content, and abrasiveness, as well as the operational requirements, such as space constraints and maintenance capabilities, when making a decision. By carefully evaluating these factors, businesses can select a conveying system that maximizes efficiency, reduces costs, and ensures the quality of their final product. Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, offers a range of conveying systems tailored to meet the diverse needs of the milling and processing industries. With years of experience and expertise, HeadPowder provides customized solutions that enhance productivity and ensure product integrity, helping businesses achieve their operational goals efficiently and effectively.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu