Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Sodium bicarbonate, commonly known as baking soda, is a versatile chemical compound widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. The efficient and safe delivery of this powder is crucial for maintaining product quality and operational efficiency. Among the various methods available for transporting sodium bicarbonate, pneumatic conveying stands out as a preferred choice for many applications due to its unique advantages and features.
Traditional vs. Modern Delivery Methods for Sodium Bicarbonate
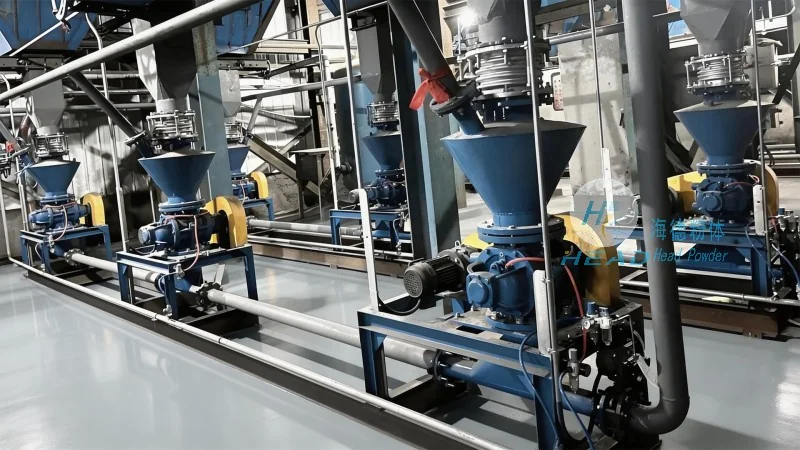
Historically, sodium bicarbonate has been transported using conventional methods such as belt conveyors, screw conveyors, and bucket elevators. These systems have been reliable for many years but often face challenges like material degradation, contamination, and limited flexibility in handling different particle sizes. For instance, belt conveyors may cause friction and abrasion, leading to product degradation, while screw conveyors can be prone to clogging, especially with fine powders like sodium bicarbonate. These traditional methods also require regular maintenance and cleaning to prevent cross-contamination, which can be time-consuming and costly.
Pneumatic Conveying: A Superior Solution for Sodium Bicarbonate Transport
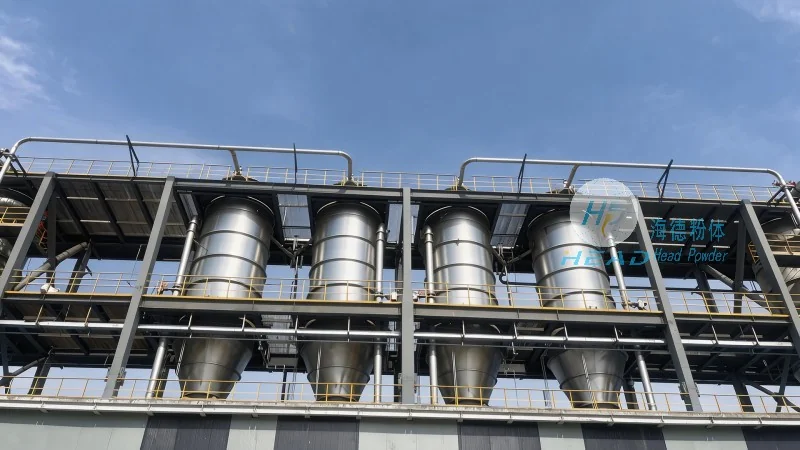
Pneumatic conveying, also known as air conveying, offers a more advanced and efficient approach to transporting sodium bicarbonate. This method involves the use of compressed air to move the powder through a pipeline system. The key advantages of pneumatic conveying for sodium bicarbonate include its ability to handle fine powders without degradation, minimal product contamination, and the flexibility to transport materials over long distances with minimal loss. Unlike mechanical systems, pneumatic conveying does not involve direct contact between the powder and the conveying equipment, reducing the risk of product contamination and ensuring a cleaner delivery process.
Key Advantages of Pneumatic Conveying for Sodium Bicarbonate
One of the primary benefits of pneumatic conveying is its ability to maintain the integrity of the sodium bicarbonate powder. The absence of mechanical components that could cause abrasion or friction ensures that the powder remains in its original state, preserving its quality and effectiveness. This is particularly important in industries where the purity of the powder is critical, such as in pharmaceutical manufacturing or food processing. Additionally, pneumatic conveying systems are highly flexible, allowing for changes in the delivery route or capacity without major modifications to the infrastructure. This adaptability makes them suitable for various production environments and scaling up operations as needed.
Another significant advantage is the cleanliness and hygiene of pneumatic conveying systems. Since the powder is transported within a sealed pipeline, there is no exposure to external contaminants, reducing the risk of cross-contamination and ensuring compliance with stringent industry standards. This is especially beneficial in food and pharmaceutical applications where product purity is paramount. Furthermore, pneumatic conveying can handle a wide range of particle sizes and flow rates, making it versatile for different production requirements. The system can be designed to accommodate varying volumes and particle characteristics, ensuring consistent performance and reliability.
Efficiency and Cost-Effectiveness in Sodium Bicarbonate Handling
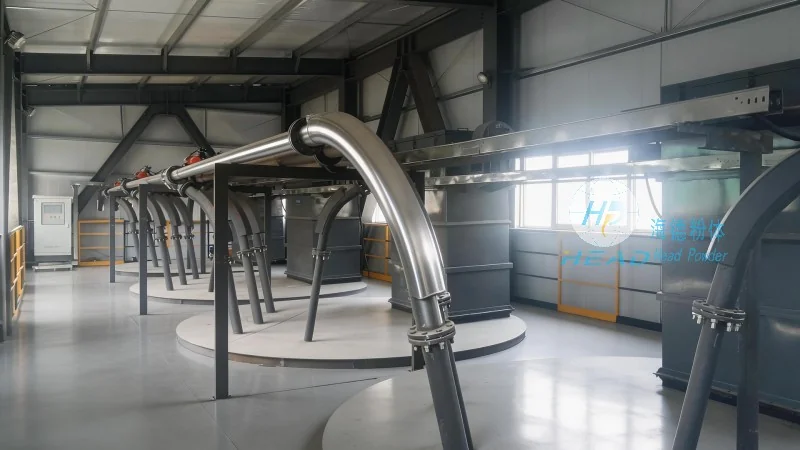
Pneumatic conveying also offers enhanced operational efficiency and cost savings compared to traditional methods. By eliminating the need for multiple transfer points and mechanical components, the system reduces downtime and maintenance costs. The ability to transport sodium bicarbonate over long distances with minimal loss of material further improves overall efficiency. Additionally, the sealed pipeline design minimizes dust emissions, contributing to a safer working environment and reduced environmental impact. These factors collectively contribute to a more economical and sustainable approach to handling sodium bicarbonate, making it an attractive option for businesses looking to optimize their operations.
HeadPowder: Expert in Pneumatic Conveying Solutions for Sodium Bicarbonate
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions, specializes in designing and implementing advanced pneumatic conveying systems tailored to the specific needs of sodium bicarbonate handling. With a strong focus on quality and innovation, HeadPowder leverages its expertise to deliver customized solutions that enhance the efficiency and safety of sodium bicarbonate transport. The company’s commitment to using high-quality materials and advanced technology ensures that its systems meet the highest industry standards and provide long-term reliability. Based in China, HeadPowder serves clients globally, offering comprehensive support from system design to installation and maintenance. By partnering with HeadPowder, businesses can benefit from optimized sodium bicarbonate delivery processes that improve productivity, reduce costs, and ensure product quality.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu