Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
When it comes to the efficient handling and transportation of corn kernels, selecting the right conveying method is crucial for optimizing production processes in agricultural and food processing industries. Various technologies are available, each with distinct advantages and applications. This article explores the primary methods used for corn kernel conveying, highlighting their functionalities and suitability for different operational needs.
1. Screw Conveyors for Corn Kernel Transport
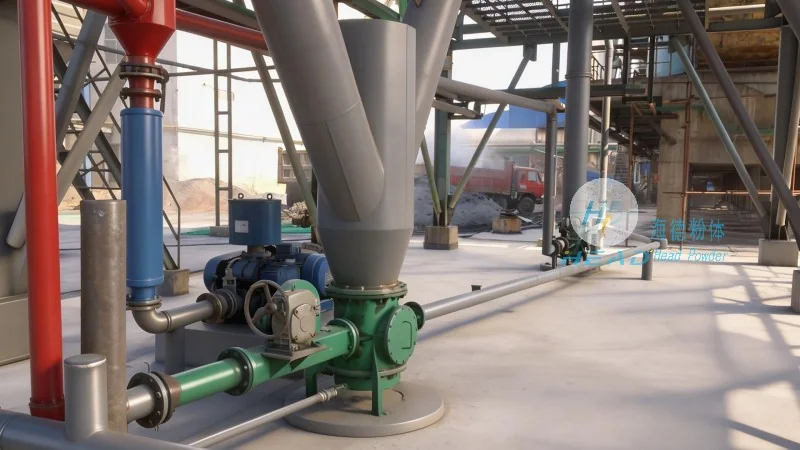
Screw conveyors, also known as auger conveyors, are among the most common and versatile equipment for moving corn kernels. These systems consist of a rotating helical screw blade enclosed within a tube or trough. As the screw rotates, it pushes the corn kernels forward along the conveyor path. Screw conveyors are particularly effective for vertical or inclined transport, making them ideal for elevating corn from storage bins to processing areas or for moving kernels between different levels in a facility. They are also suitable for handling bulk materials with minimal spillage, as the enclosed design helps contain the product. The design of screw conveyors can be customized to accommodate varying kernel sizes and moisture content, ensuring efficient operation without causing damage to the kernels. This makes them a reliable choice for continuous corn kernel conveying in agricultural processing plants.
2. Pneumatic Conveying Systems for Corn Kernels
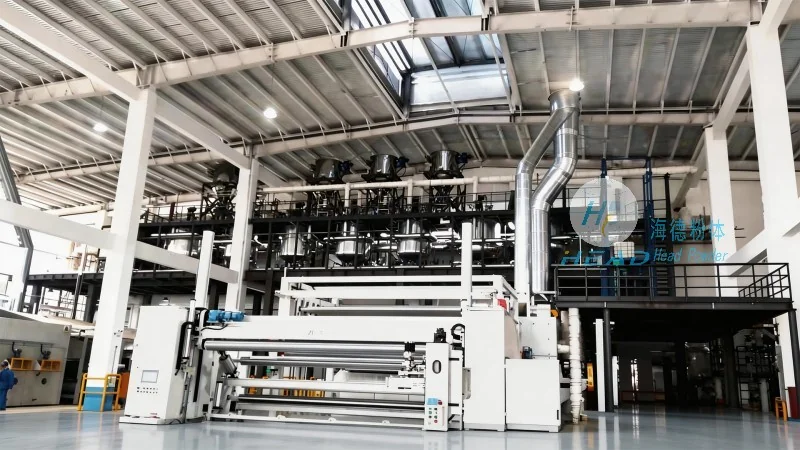
Pneumatic conveying systems utilize air or gas to transport corn kernels through a network of pipes. These systems can be categorized into two main types: pressure and vacuum. In pressure systems, air is blown into a sealed pipe, creating a positive pressure that pushes the corn kernels forward. Vacuum systems, on the other hand, use suction to draw the kernels into the pipe. Pneumatic conveyors are highly effective for long-distance transport, as they can move corn kernels over several hundred meters without the need for multiple transfer points. They are also beneficial for handling fine or delicate kernels, as the enclosed air flow minimizes breakage and dust generation. Additionally, these systems can be integrated with other processing equipment, such as cleaning or sorting machines, to create a seamless material flow. Pneumatic conveying is particularly advantageous in environments where hygiene and contamination control are critical, as the enclosed system prevents exposure to external elements. However, it is important to note that these systems require proper maintenance to ensure consistent performance and to prevent air leaks that could affect conveying efficiency.
3. Belt Conveyors for Bulk Corn Kernel Handling
Belt conveyors are another widely used method for conveying corn kernels, especially in large-scale agricultural operations. These systems consist of a continuous belt that moves over rollers or a flat surface, transporting the kernels from one location to another. Belt conveyors are capable of handling high volumes of corn kernels and are suitable for both horizontal and slight incline transport. They are often used in combination with other equipment, such as hoppers or feeders, to ensure a steady flow of material. The design of belt conveyors can be customized to accommodate different kernel sizes and moisture levels, making them adaptable to various processing requirements. One of the key advantages of belt conveyors is their ability to handle a wide range of materials, including wet or sticky kernels, without causing significant wear or damage to the conveyor components. This makes them a durable and reliable option for long-term corn kernel transport in processing facilities. Additionally, belt conveyors can be equipped with sensors and controls to monitor the flow rate and detect any blockages, enhancing operational safety and efficiency.
4. Bucket Elevators for Vertical Corn Kernel Transport
Bucket elevators are specialized equipment designed for vertical transport of corn kernels, often used in conjunction with other conveying systems to move kernels from ground level to elevated storage or processing areas. These systems consist of a vertical or slightly inclined conveyor with a series of buckets attached to a chain or belt. As the buckets rotate and move upward, they scoop up the corn kernels and discharge them at the top of the elevator. Bucket elevators are highly efficient for vertical transport, as they can move large quantities of kernels at a high speed with minimal energy consumption. They are particularly effective for handling bulk materials that require vertical movement, such as corn kernels from storage silos to processing lines. The design of bucket elevators allows for customization based on the kernel size and density, ensuring optimal performance. One of the main advantages of bucket elevators is their ability to handle high volumes of material with low maintenance requirements, making them a cost-effective solution for vertical corn kernel conveying. However, it is important to ensure proper alignment and tensioning of the buckets to prevent material spillage and maintain efficient operation.
5. Vibrating Conveyors for Gentle Corn Kernel Handling
Vibrating conveyors are a gentler alternative to other conveying methods, designed to minimize kernel damage during transport. These systems use vibration to move corn kernels along a trough or conveyor bed. The vibration is typically generated by an electric motor connected to a drive system, which causes the conveyor to oscillate at a specific frequency. This gentle motion helps move the kernels forward without applying excessive force, reducing the risk of breakage or bruising. Vibrating conveyors are particularly suitable for handling delicate or high-value corn kernels, such as those intended for human consumption or seed production. They are also effective for transporting kernels with high moisture content or sticky characteristics, as the vibration helps prevent material buildup and ensures smooth flow. The design of vibrating conveyors can be adjusted to accommodate different kernel sizes and flow rates, making them versatile for various processing applications. Additionally, these systems are easy to clean and maintain, which is beneficial in food processing environments where hygiene is a priority. Vibrating conveyors are often used in combination with other equipment, such as screening or sorting machines, to create a seamless material handling process.
6. Choosing the Right Conveying Method for Corn Kernels
When selecting a conveying method for corn kernels, several factors must be considered to ensure optimal performance and efficiency. These factors include the volume of kernels to be transported, the distance between the source and destination, the required speed of transport, and the characteristics of the kernels (such as size, moisture content, and density). Each conveying method has its strengths and limitations, and the choice should align with the specific operational needs of the facility. For example, screw conveyors are ideal for vertical or inclined transport of bulk kernels, while pneumatic systems are better suited for long-distance or high-volume transport. Belt conveyors are suitable for large-scale horizontal transport, and bucket elevators are effective for vertical movement. Vibrating conveyors offer a gentle alternative for delicate kernels. It is also important to consider the cost of installation, maintenance, and energy consumption when evaluating different options. By carefully assessing these factors, agricultural and food processing facilities can select the most appropriate conveying method to enhance productivity and ensure the quality of their corn kernel products.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of conveying solutions, specializes in designing and manufacturing equipment tailored to the unique needs of corn kernel handling. With years of experience in the industry, the company offers a range of conveying systems, including screw conveyors, pneumatic systems, belt conveyors, and bucket elevators, to meet the diverse requirements of agricultural processing operations. Based in China, Shandong HeadPowder Engineering Co., Ltd. leverages advanced technology and engineering expertise to deliver reliable and efficient conveying solutions that enhance productivity and ensure the quality of corn kernel products. The company's commitment to quality and customer satisfaction has made it a trusted partner for facilities worldwide, helping them optimize their corn kernel handling processes and improve overall operational efficiency.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu