Công ty Hải Đức Bột với hơn 10 năm kinh nghiệm vận chuyển khí, cung cấp hệ thống‑thiết bị‑quạt gió và nhận dự án tổng thầu bột cả nước
Pharmaceutical manufacturing relies on efficient and reliable material handling systems to ensure product quality, safety, and regulatory compliance. Among the various methods used for transporting powders and bulk materials in pharmaceutical settings, pneumatic conveying stands out as a preferred solution due to its unique advantages and technical capabilities. This article explores the different pharmaceutical conveying methods available, with a focus on the benefits and characteristics of pneumatic conveying systems.
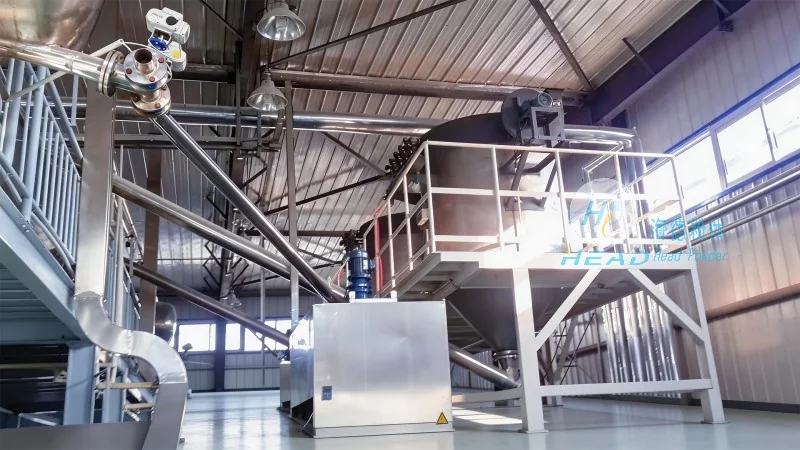
Understanding Pharmaceutical Conveying Methods
In the pharmaceutical industry, the selection of an appropriate conveying method is critical as it directly impacts product integrity, operational efficiency, and adherence to stringent quality standards. Conventional methods such as belt conveyors, screw conveyors, and bucket elevators have been widely used, but they often face challenges like material contamination, product degradation, and difficulty in handling fine powders. Pneumatic conveying, however, addresses these issues by utilizing air or gas to transport materials in a closed system, minimizing exposure to external contaminants and maintaining product purity.
Pneumatic Conveying Systems: Key Advantages
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying solutions tailored for pharmaceutical applications. The primary advantages of pneumatic conveying systems in pharmaceutical manufacturing include:
Hygienic and Clean Operation: Pneumatic systems operate in a closed loop, preventing cross-contamination between different product batches and reducing the risk of microbial growth. This is crucial for maintaining the sterility and purity of pharmaceutical products.
Flexibility and Versatility: These systems can handle a wide range of materials, from fine powders to bulk solids, and can be easily reconfigured to accommodate changes in production processes or product lines.
Energy Efficiency: Compared to mechanical conveyors, pneumatic systems often require less energy to transport materials over short to medium distances, leading to lower operational costs and reduced environmental impact.
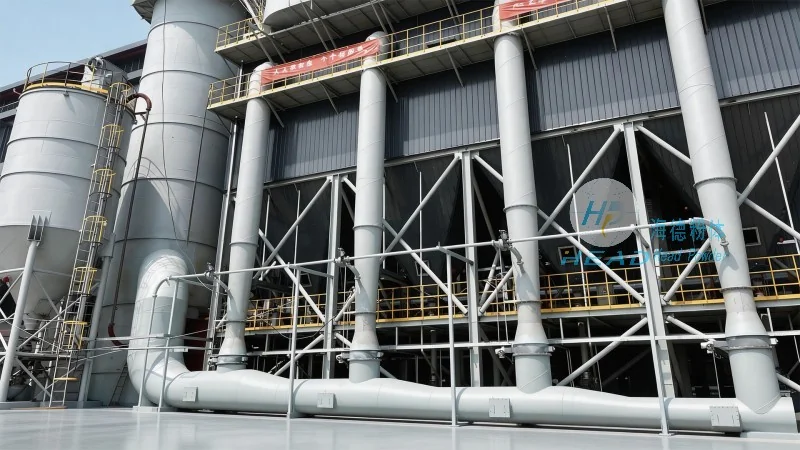
Space Efficiency: Pneumatic conveying systems are compact and can be installed in limited spaces, making them ideal for facilities with constrained layouts or where space optimization is a priority.
Reduced Product Degradation: The enclosed nature of the system minimizes exposure to air, light, and moisture, which can cause degradation or oxidation of sensitive pharmaceutical ingredients.
Technical Features of Pneumatic Conveying
HeadPowder’s pneumatic conveying systems are engineered with precision to meet the demanding requirements of the pharmaceutical industry. Key technical features include:
Positive Displacement Pumps: These pumps ensure consistent and controlled material flow, preventing clogging and maintaining uniform product distribution.
Filter and Dust Collection Systems: Advanced filtration technologies are integrated to capture fine particles and maintain air quality, ensuring compliance with environmental regulations and product safety standards.
Controlled Airflow and Pressure: Precise control of air pressure and flow rate allows for accurate material transfer, reducing waste and optimizing process efficiency.
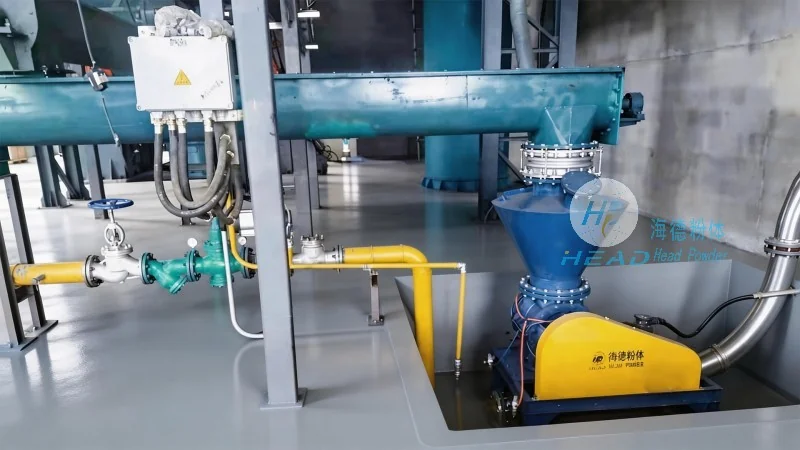
Material Compatibility: Components are made from materials such as stainless steel, PTFE, and food-grade plastics to prevent chemical reactions or contamination with pharmaceutical products.
Applications in Pharmaceutical Manufacturing
Pneumatic conveying systems are widely used in various stages of pharmaceutical production, including:
Raw Material Handling: Transporting raw powders from storage silos to processing lines.
Intermediate Product Transfer: Moving finished intermediates between different production units without exposing them to external contaminants.
Finished Product Packaging: Conveying final products to packaging lines for final labeling and distribution.
Waste Management: Efficiently handling waste materials while maintaining hygiene standards.
Conclusion
As the pharmaceutical industry continues to prioritize quality, safety, and efficiency, pneumatic conveying systems offer a reliable and advanced solution for material handling. HeadPowder Engineering Co., Ltd., with its expertise and commitment to innovation, provides customized pneumatic conveying solutions that meet the unique needs of pharmaceutical manufacturers. Based in Shandong, China, the company leverages its technical knowledge and manufacturing capabilities to deliver high-quality systems that enhance operational performance and ensure product integrity.

 Công ty TNHH Kỹ thuật Công trình Bột Hải Đức Sơn Đông
 156-6277-7102(Quản lý Trương)
 0531-83386006
 Quận Chương Khâu, Thành phố Tế Nam, Tỉnh Sơn Đông, Trung Quốc

Điện thoại
WeChatTư vấn
Lên đầu